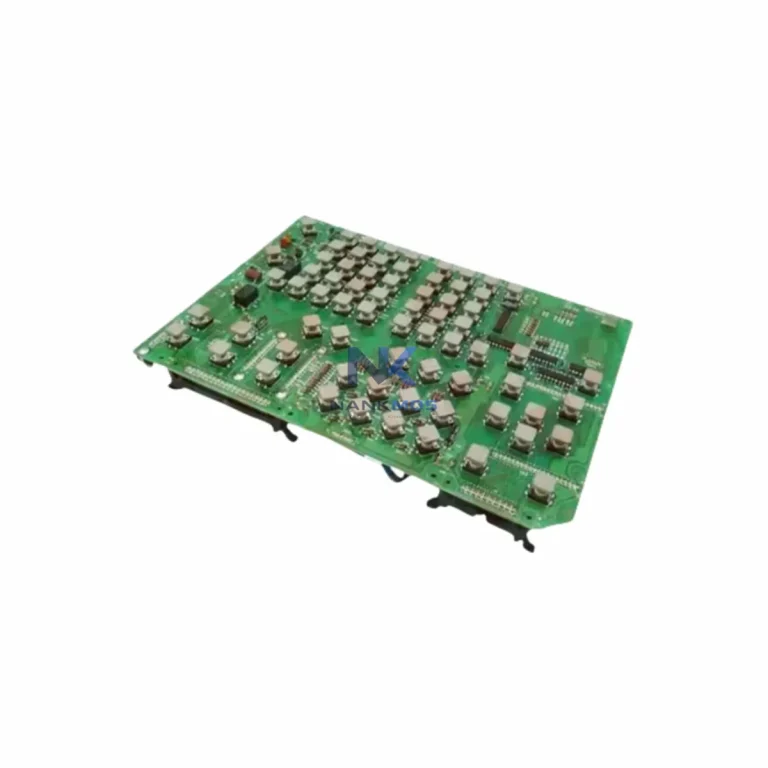
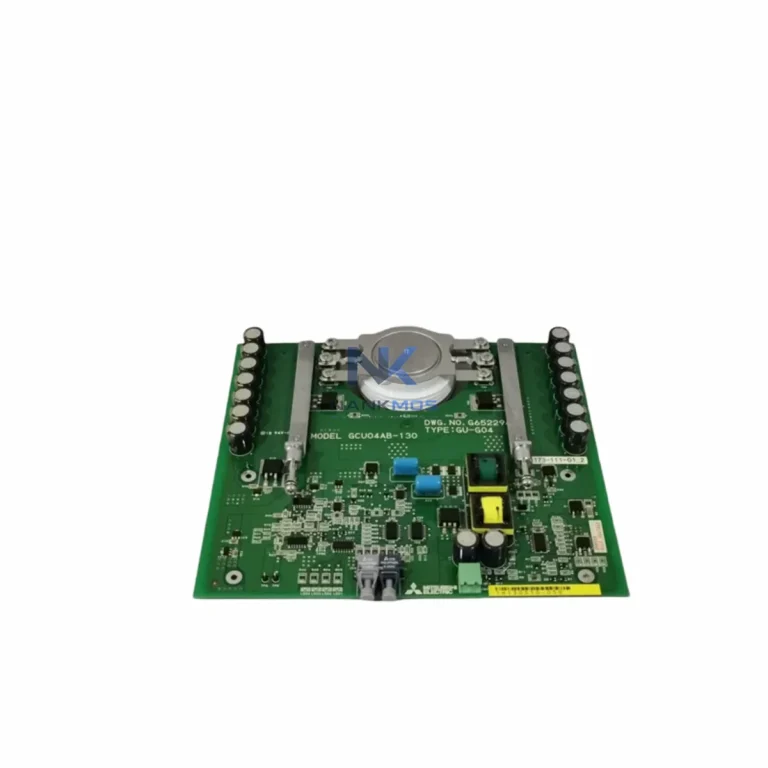
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
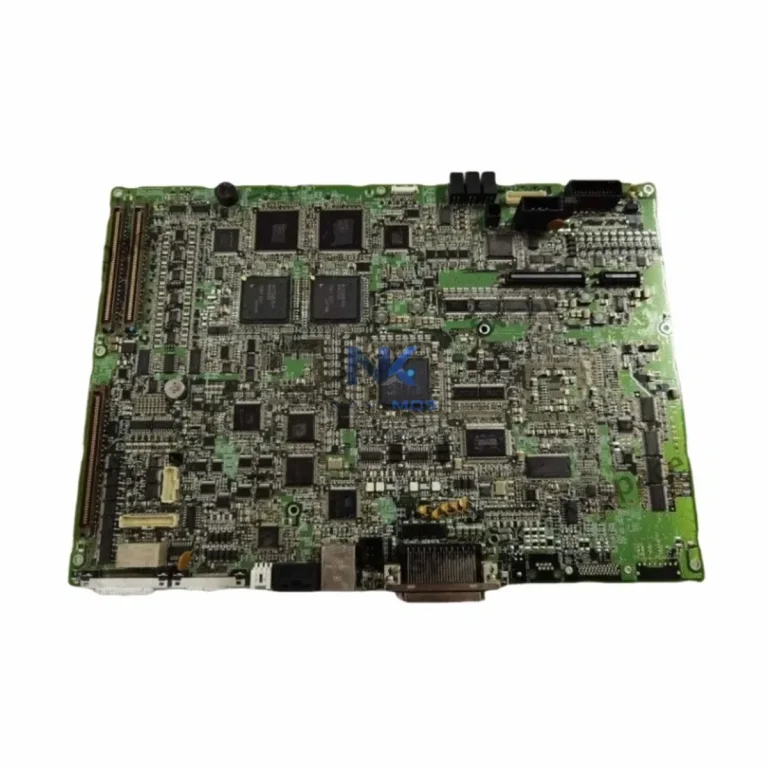
MITSUBISHI FX61C BN624A551G51 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.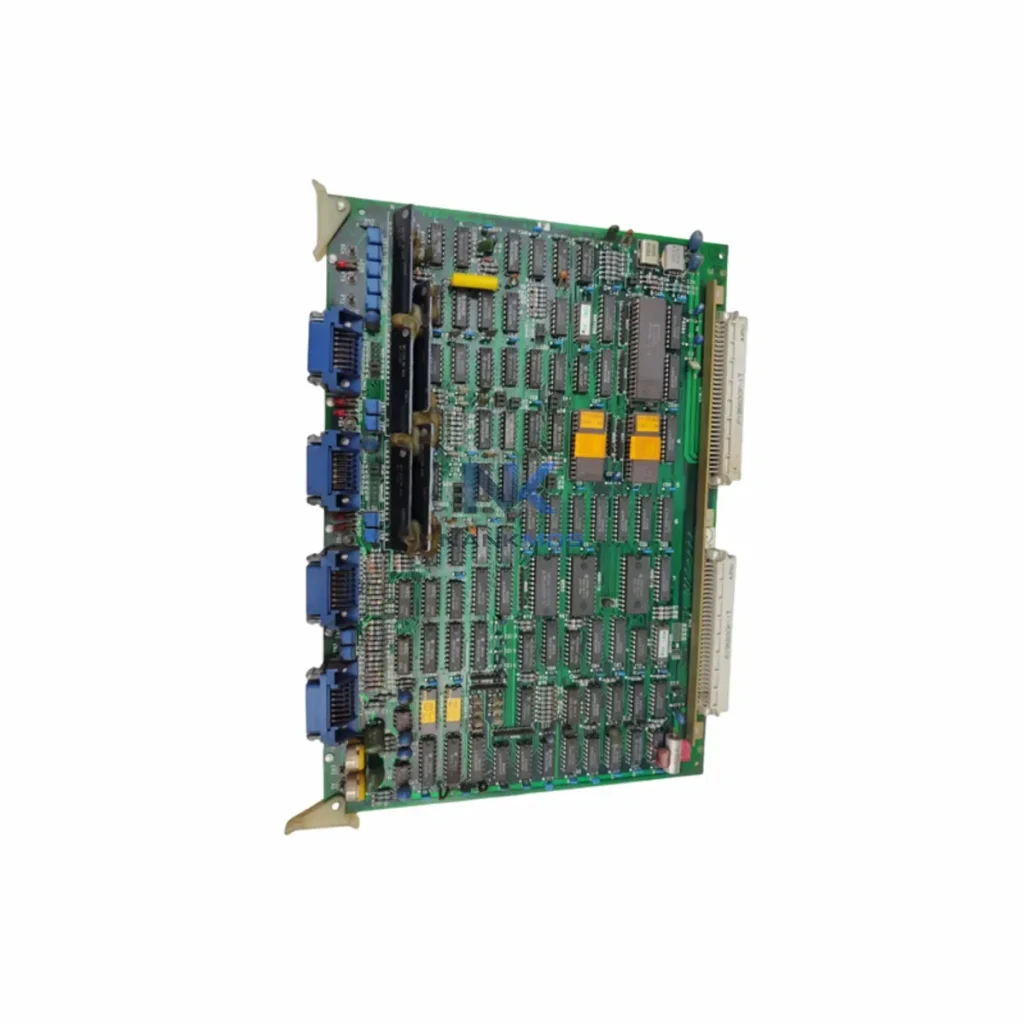
MITSUBISHI FX61C BN624A551G51 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | MITSUBISHI |
|---|---|
| Application | Industrial Network Communication |
| Part Number / Model | FX61C BN624A551G51 |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Communication Module |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The Mitsubishi FX61C BN624A551G51 is a high-performance industrial network interface and CNC communication board engineered for MELDAS-series CNC controllers. Designed to bridge the gap between legacy CNC machine tools and modern smart factory architectures, this module enables seamless protocol conversion, real-time data acquisition, and reliable network communication across multi-vendor automation environments. Whether integrating with SCADA platforms, HMI terminals, or upper-level MES systems, the FX61C BN624A551G51 delivers the connectivity backbone that modern production lines demand.
In today's data-driven manufacturing landscape, every CNC axis, spindle signal, and alarm event carries operational intelligence. The FX61C BN624A551G51 captures this intelligence at the source — within the MELDAS CNC controller — and transmits it upstream through standardised industrial communication channels. This makes it an indispensable component for factories pursuing real-time production transparency, predictive maintenance, and remote diagnostics.
The FX61C BN624A551G51 sits at the heart of a layered industrial data architecture. At the field level, MELDAS CNC controllers govern machining operations — managing servo axes, spindle drives, and tool change sequences. The FX61C communication board extracts live operational data from the CNC backplane and routes it through serial communication channels toward the network layer.
In a typical smart factory deployment, the FX61C BN624A551G51 connects to an industrial serial-to-Ethernet gateway — such as a Mitsubishi MR-J4 series gateway module or a third-party protocol converter — which translates MELDAS serial data into Ethernet-compatible frames. From there, data flows into a managed industrial Ethernet switch (e.g., a 24-port DIN-rail switch with PROFINET or EtherNet/IP support), distributing signals across the plant network to SCADA servers, HMI panels, and MES platforms.
On the control side, Mitsubishi MELSEC Q-series or iQ-R series PLCs may operate in parallel with the CNC system, handling peripheral I/O — conveyor interlocks, coolant control, part-present sensors — via remote I/O modules such as the Mitsubishi QJ71E71 Ethernet interface or AJ65BT-64AD analogue input module. These PLC nodes feed their data into the same plant network, creating a unified data fabric that the SCADA layer can query in real time.
HMI terminals — such as Mitsubishi GOT2000 series panels — display live CNC status, alarm histories, and production counts sourced directly from the FX61C communication board's data stream. Operators on the shop floor gain immediate visibility into axis positions, feed rates, and fault codes without leaving the machine cell. Meanwhile, SCADA platforms (e.g., Wonderware, iFIX, or Mitsubishi GENESIS64) aggregate data from multiple CNC nodes, PLCs, and remote I/O stations into unified dashboards, enabling shift supervisors to monitor OEE, cycle times, and alarm frequencies across the entire production line.
For facilities integrating variable frequency drives (VFDs) on auxiliary equipment — such as Mitsubishi FR-A800 series inverters controlling coolant pumps or chip conveyors — the same network infrastructure carries drive status, fault registers, and energy consumption data alongside CNC telemetry. Edge gateway devices at the network boundary perform local data pre-processing, buffering CNC and drive data before forwarding aggregated records to cloud-based MES or ERP systems, ensuring low-latency local control is never compromised by upstream network congestion.
Industrial power supplies (e.g., Mitsubishi Q61P or equivalent DIN-rail PSUs) provide stable 24 VDC to the communication board and associated network hardware, while signal isolators and surge protection modules safeguard the serial communication lines from electrical noise common in high-power machining environments. The result is a robust, end-to-end data chain — from CNC spindle signal to SCADA dashboard — anchored by the FX61C BN624A551G51 at the field edge.
Protocol Fragmentation: Many production sites operate a mix of legacy MELDAS CNC controllers alongside newer FANUC, Siemens, or Mitsubishi MELSEC-based systems. The FX61C BN624A551G51 addresses this by providing a standardised serial communication interface that can be bridged to modern protocol converters, eliminating the data silos that arise when proprietary CNC protocols cannot communicate with plant-wide Ethernet networks.
Data Islands and Production Opacity: Without a dedicated communication board, CNC machine data remains locked inside the controller — invisible to SCADA, MES, and management dashboards. The FX61C BN624A551G51 unlocks this data, enabling production counts, cycle times, alarm events, and axis diagnostics to flow continuously into upper-level systems. Shift managers gain real-time production transparency without relying on manual operator reports.
Remote Monitoring and Diagnostics: When a CNC alarm occurs at 2:00 AM, the FX61C's data stream allows SCADA systems to log the exact fault code, axis state, and timestamp — enabling maintenance engineers to diagnose the root cause remotely before arriving on-site. This capability dramatically reduces mean time to repair (MTTR) and minimises unplanned downtime on critical machining cells.
Alarm Tracking and Escalation: Integrated with SCADA alarm management modules, the FX61C BN624A551G51 supports structured alarm logging, escalation workflows, and historical trend analysis. Recurring faults — such as servo overload alarms on a specific axis — can be identified and addressed proactively, shifting maintenance strategy from reactive to predictive.
System Scalability: As production capacity grows, additional MELDAS CNC nodes can be networked using the same FX61C communication board architecture, with each node feeding into the shared plant Ethernet infrastructure. This modular approach ensures that the smart factory data layer scales linearly with the number of machine tools, without requiring architectural redesign.
Q1: What communication protocols does the Mitsubishi FX61C BN624A551G51 support? The FX61C BN624A551G51 is a MELDAS-series CNC communication board that supports the proprietary MELDAS serial communication protocol, with RS-232C and RS-422 physical interfaces. For integration with modern Ethernet-based SCADA or MES systems, a serial-to-Ethernet protocol gateway is used in conjunction with this board. This approach ensures compatibility with a wide range of supervisory platforms without modifying the CNC controller's core firmware.
Q2: How does this board ensure network stability in high-noise machining environments? The FX61C BN624A551G51 is designed for industrial-grade reliability within the MELDAS CNC controller backplane. Serial communication lines should be routed with appropriate shielding and surge protection to mitigate EMI from servo drives, spindle motors, and high-frequency cutting equipment. When paired with industrial-grade serial isolators and managed Ethernet switches with storm control, the communication link maintains stable, low-latency data transmission even in electrically demanding environments.
Q3: Can this module support remote diagnostics and SCADA integration simultaneously? Yes. The FX61C BN624A551G51 continuously streams CNC status, alarm codes, axis positions, and I/O states through its serial interface. When connected via a protocol gateway to a plant Ethernet network, this data is simultaneously available to SCADA platforms for real-time monitoring, HMI panels for operator display, and remote diagnostic tools for maintenance engineers — all without interrupting the CNC machining cycle.
Q4: What warranty and pre-shipment testing does NANKMOS provide for this product? All Mitsubishi FX61C BN624A551G51 units supplied by NANKMOS are covered by a 12-Month Warranty and undergo pre-shipment functional testing to verify communication board integrity and interface continuity. In-stock units are available for immediate dispatch. For volume orders, lead time and availability can be confirmed by contacting our technical sales team directly.
Functional Inspection100% tested on professional platforms to ensure stable performance.
 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.