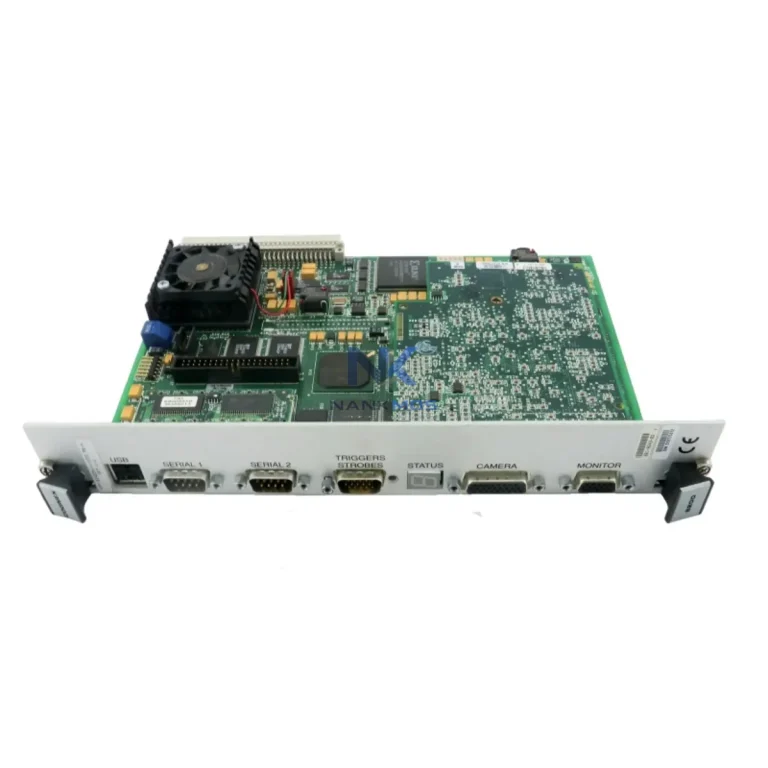
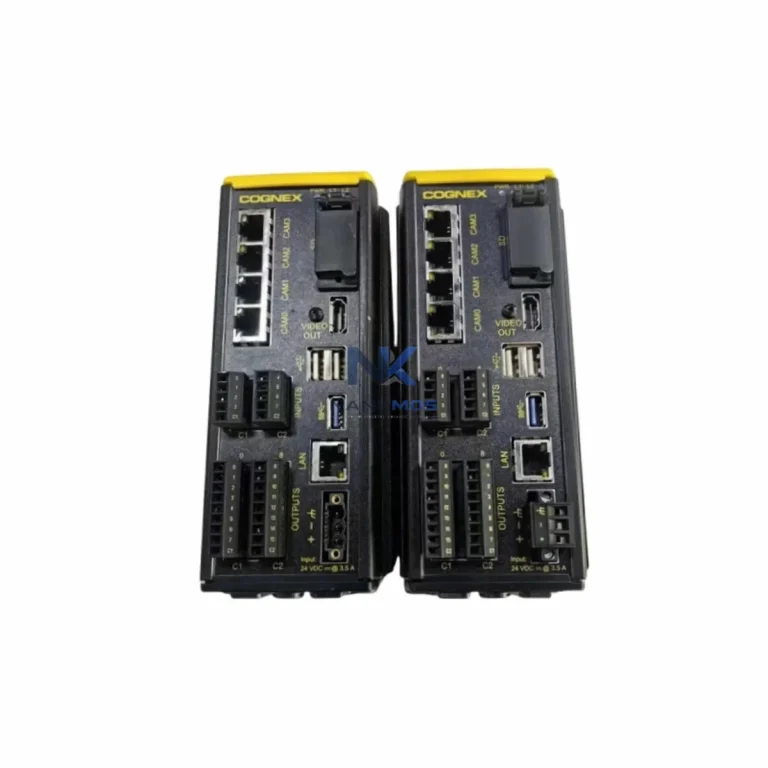
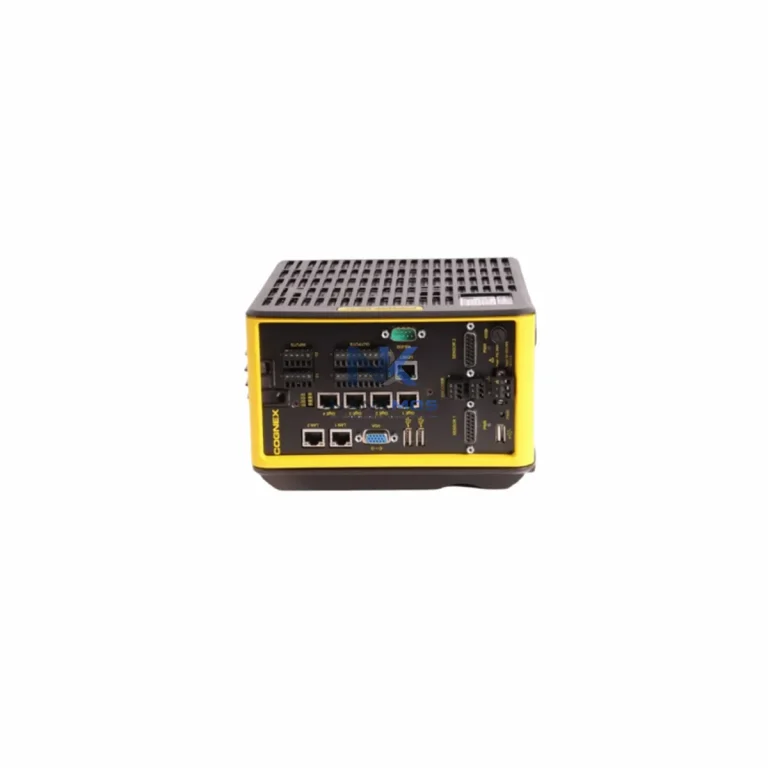
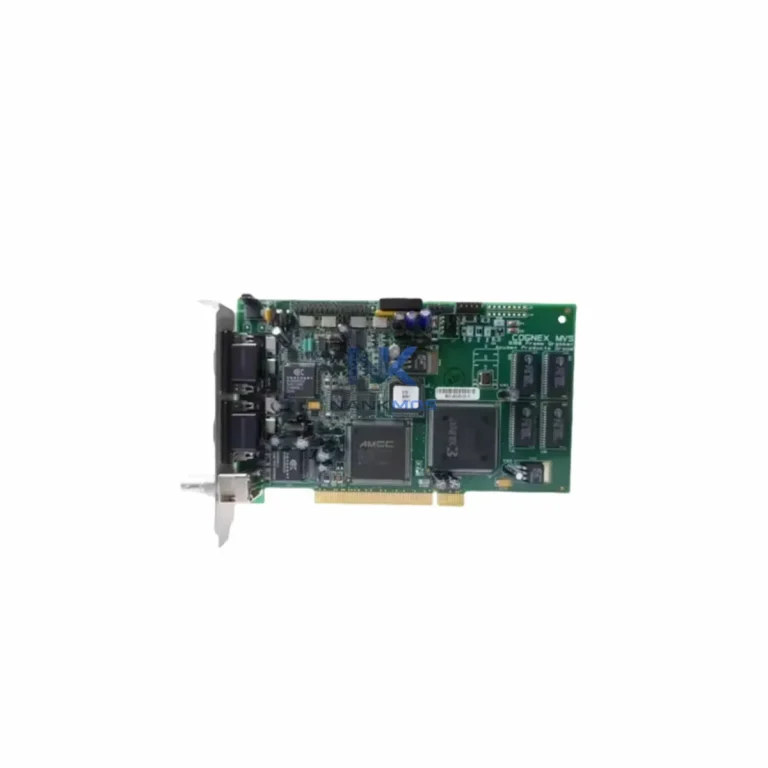
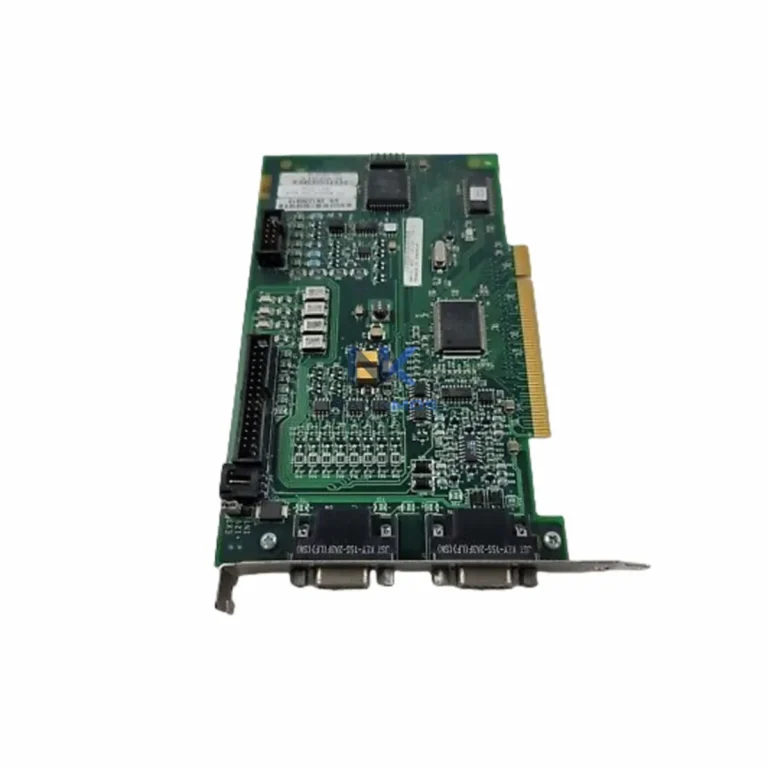
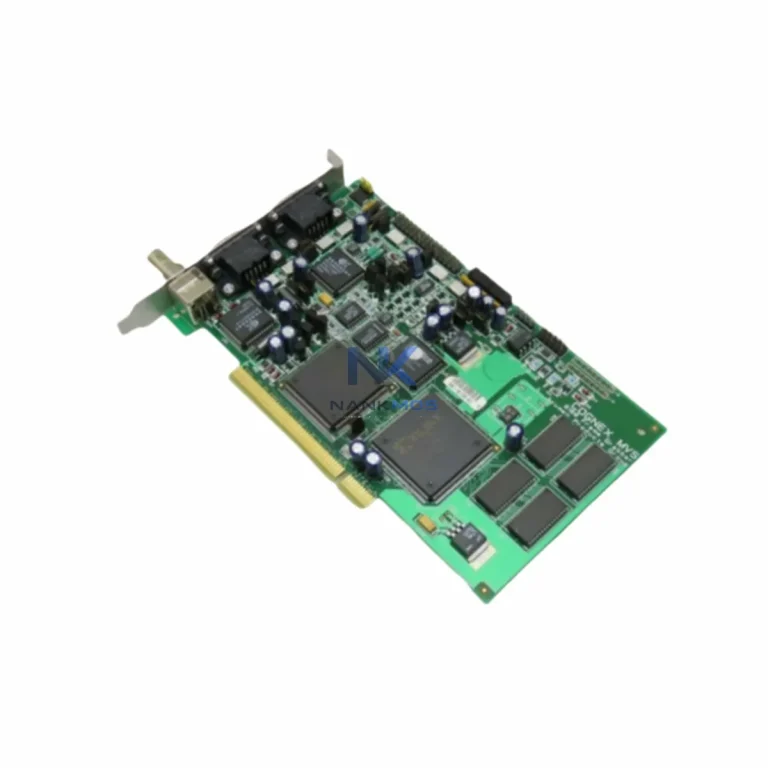
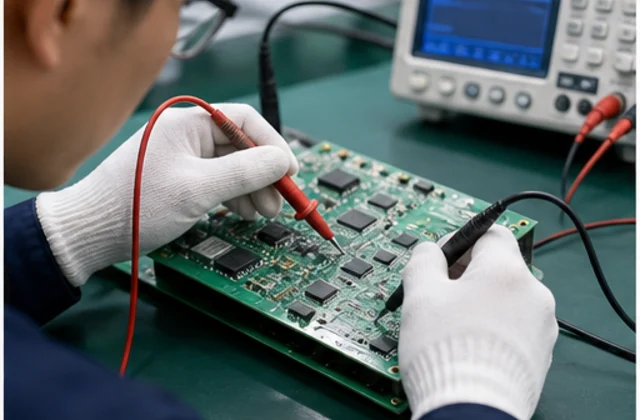
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
Cognex VPM-8120X-5061-P is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices > Programmable Logic Controllers. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.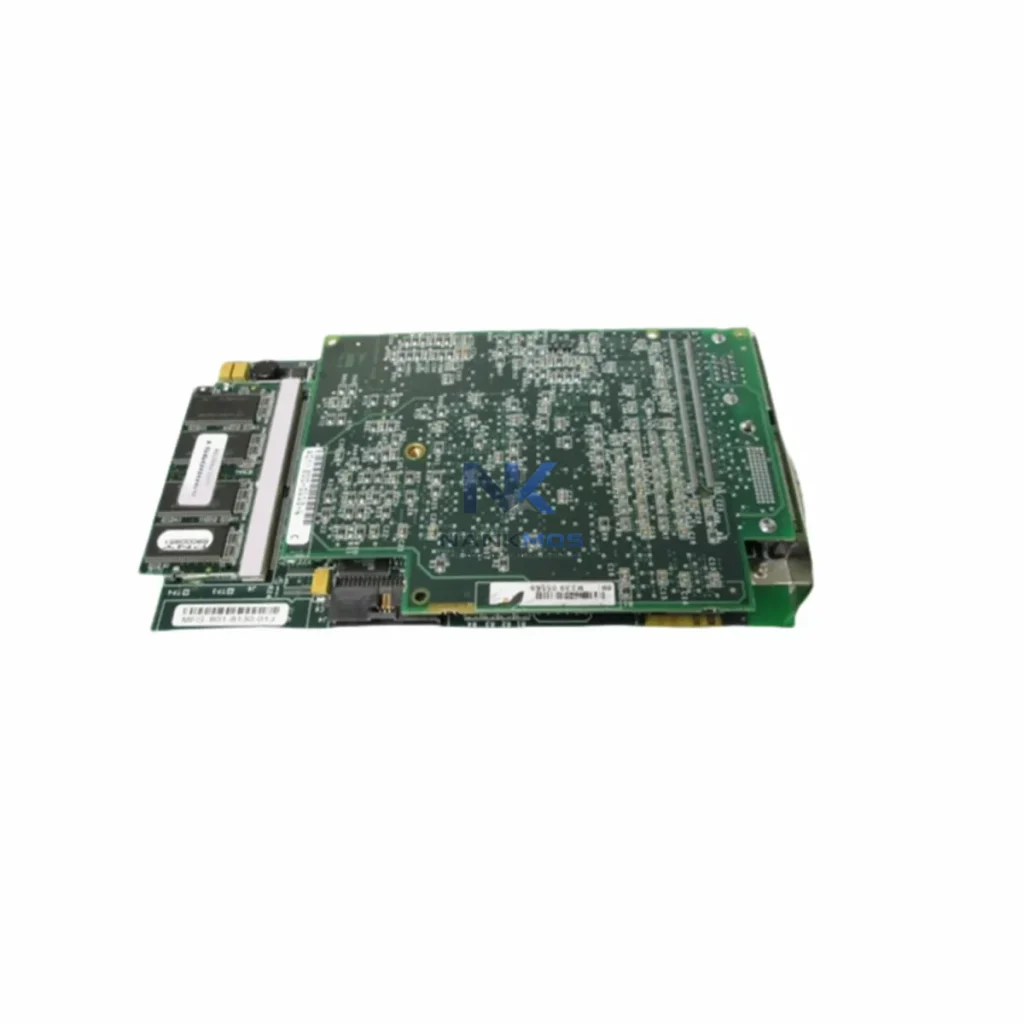
Cognex VPM-8120X-5061-P is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices > Programmable Logic Controllers. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | Cognex |
|---|---|
| Application | Controller Processing & System Control |
| Part Number / Model | VPM-8120X-5061-P |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Controller / CPU Module |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The Cognex VPM-8120X-5061-P is a high-performance vision processor module engineered to serve as a critical data link node within modern smart factory architectures. Designed for demanding industrial environments, this unit bridges machine vision intelligence with plant-wide automation networks through native support for EtherNet/IP, PROFINET, Modbus TCP, and OPC-UA — four of the most widely deployed industrial communication protocols in discrete manufacturing, automotive assembly, electronics production, and process automation.
In a connected factory, data does not stop at the camera lens. The VPM-8120X-5061-P captures inspection results, dimensional measurements, barcode reads, and pass/fail decisions at the vision layer, then transmits structured data packets upstream to PLCs, SCADA servers, MES platforms, and HMI terminals in real time. This seamless data flow eliminates the traditional gap between vision systems and control networks, enabling operators to act on quality intelligence the moment it is generated on the production line.
Understanding the VPM-8120X-5061-P requires viewing it not as a standalone device, but as a node within a layered industrial data architecture. At the field level, Cognex vision sensors and smart cameras — such as units from the In-Sight 9000 series — capture raw image data and perform on-device inspection logic. The VPM-8120X-5061-P acts as the processing and communication hub, aggregating results from multiple vision nodes and formatting them for network transmission.
On the control layer, the module communicates directly with Rockwell Automation ControlLogix L8x PLCs via EtherNet/IP, delivering inspection tags — pass/fail bits, measurement values, and fault codes — into the PLC's data table without requiring custom middleware. Simultaneously, PROFINET connectivity allows integration with Siemens S7-1500 series controllers, making the VPM-8120X-5061-P equally at home in European-standard automation environments. For legacy systems or mixed-vendor lines, Modbus TCP provides a universal fallback, enabling communication with Schneider Electric Modicon M340 PLCs, remote I/O racks, and third-party motion controllers.
Moving up the network stack, OPC-UA connectivity opens a direct channel to SCADA platforms such as Ignition by Inductive Automation, Wonderware AVEVA System Platform, and Siemens WinCC. Vision data — including inspection counts, defect rates, cycle times, and traceability records — flows continuously into SCADA historian databases, where it becomes available for real-time dashboards, SPC charting, and production KPI reporting. HMI terminals on the shop floor, whether panel-mounted units from Siemens, Weintek, or Advantech, can subscribe to OPC-UA data nodes published by the VPM-8120X-5061-P, giving line operators live visibility into inspection status without requiring PLC intermediaries.
At the edge layer, the module's data output can be consumed by industrial edge gateways — such as Moxa UC-8100 series or Advantech ECU-1000 platforms — which perform local data buffering, protocol bridging, and cloud forwarding. This architecture supports hybrid deployments where time-critical control data stays on-premise while aggregated quality metrics are forwarded to cloud analytics platforms via MQTT or REST APIs. Industrial managed switches — including units from Hirschmann RS20 or Cisco IE-3000 series — provide the network backbone, ensuring deterministic packet delivery and VLAN segmentation between the vision network, control network, and enterprise IT layer.
For drive and motion integration, the VPM-8120X-5061-P can trigger servo drives and variable frequency drives (VFDs) — such as Yaskawa Sigma-7 servo amplifiers or ABB ACS880 drives — through PLC interlocks based on vision inspection results. A failed inspection result propagates through the EtherNet/IP network to the PLC, which commands the drive to halt the conveyor or divert the reject part, completing a closed-loop quality control cycle entirely within the automation network.
Power and signal integrity across this data chain is supported by industrial DIN-rail power supplies rated for 24 VDC output, ensuring the VPM-8120X-5061-P and its connected vision peripherals operate within specified voltage tolerances even in electrically noisy panel environments. The result is a complete, validated data pathway from physical inspection event to enterprise-level quality record — with the Cognex VPM-8120X-5061-P at the centre of the communication architecture.
Protocol Fragmentation: Many production sites run mixed-vendor automation environments where Rockwell PLCs coexist with Siemens controllers, legacy Modbus devices, and modern OPC-UA-capable SCADA systems. The VPM-8120X-5061-P resolves this fragmentation by natively supporting all four major industrial protocols simultaneously, eliminating the need for external protocol converters or custom integration software. Vision data is published in the correct format for each target system without manual mapping or middleware configuration.
Data Silos and Production Transparency: Vision inspection results that remain isolated within the vision system cannot contribute to production analytics, OEE calculations, or traceability records. By connecting the VPM-8120X-5061-P to SCADA and MES platforms via OPC-UA, inspection data becomes a first-class citizen in the plant data model — searchable, historised, and reportable alongside PLC cycle counts, downtime events, and material consumption records. Line managers gain real-time transparency into quality trends without waiting for end-of-shift reports.
Remote Monitoring and Diagnostics: Unplanned downtime caused by vision system faults is costly and difficult to diagnose remotely. The VPM-8120X-5061-P exposes diagnostic registers — camera connection status, processing load, communication error counts, and inspection throughput — via its network interfaces. Remote engineers can query these registers through SCADA or OPC-UA clients without physical access to the machine, enabling faster fault isolation, predictive maintenance scheduling, and reduced mean time to repair (MTTR).
Alarm Tracking and Escalation: Integrated with SCADA alarm management systems, the VPM-8120X-5061-P can trigger structured alarm events when inspection failure rates exceed configurable thresholds. These alarms propagate through the plant alarm hierarchy — from HMI operator alerts to supervisor email notifications — ensuring that quality excursions are captured, acknowledged, and resolved within defined response time windows, fully compliant with ISA-18.2 alarm management standards.
System Scalability: As production lines expand, additional vision stations can be added to the network without architectural redesign. The VPM-8120X-5061-P's multi-protocol support ensures that new stations integrate with existing PLC programs and SCADA configurations using the same tag structures and communication patterns already in use, protecting the engineering investment made during initial deployment.
Q1: What is the typical communication latency between the VPM-8120X-5061-P and a connected PLC via EtherNet/IP? Under normal network conditions with a managed industrial switch and dedicated VLAN, EtherNet/IP implicit messaging (Class 1) between the VPM-8120X-5061-P and a Rockwell ControlLogix PLC achieves cycle times of 10–20 ms, suitable for most discrete manufacturing inspection applications. Explicit messaging for configuration and diagnostics operates asynchronously and does not impact control cycle performance.
Q2: Is the VPM-8120X-5061-P compatible with both Siemens TIA Portal and Rockwell Studio 5000 engineering environments? Yes. PROFINET connectivity enables integration with Siemens TIA Portal projects using standard GSD/GSDML device description files, while EtherNet/IP support allows Add-On Profile (AOP) or generic Ethernet module configuration within Rockwell Studio 5000. Both environments can coexist on the same physical network, with the VPM-8120X-5061-P serving as a multi-protocol data source for each PLC platform independently.
Q3: How does NANKMOS verify the VPM-8120X-5061-P before shipment? Every unit undergoes a pre-shipment functional test covering power-on self-diagnostics, network interface enumeration, and protocol communication verification. Units are confirmed operational across all supported interfaces before dispatch. Full test records are available upon request. The VPM-8120X-5061-P is covered by a 12-Month Warranty from the date of delivery, with direct technical support available through NANKMOS.
Q4: Can the VPM-8120X-5061-P support remote firmware updates and configuration changes without production downtime? Remote configuration changes can be performed via OPC-UA method calls or Modbus TCP register writes during scheduled maintenance windows. Firmware update procedures follow Cognex's standard update protocol and are typically performed during planned downtime. NANKMOS technical support can assist with update planning and validation to minimise production impact.
Functional Inspection100% tested on professional platforms to ensure stable performance.
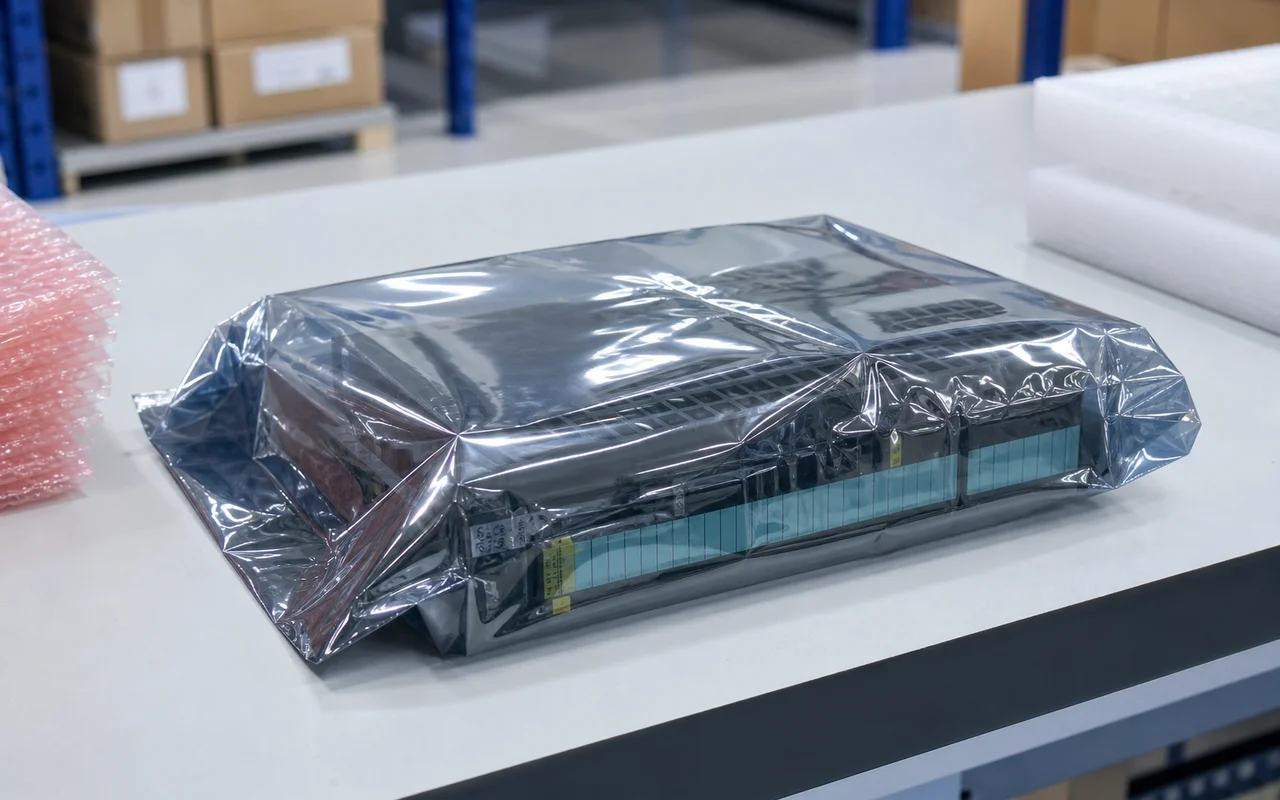 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
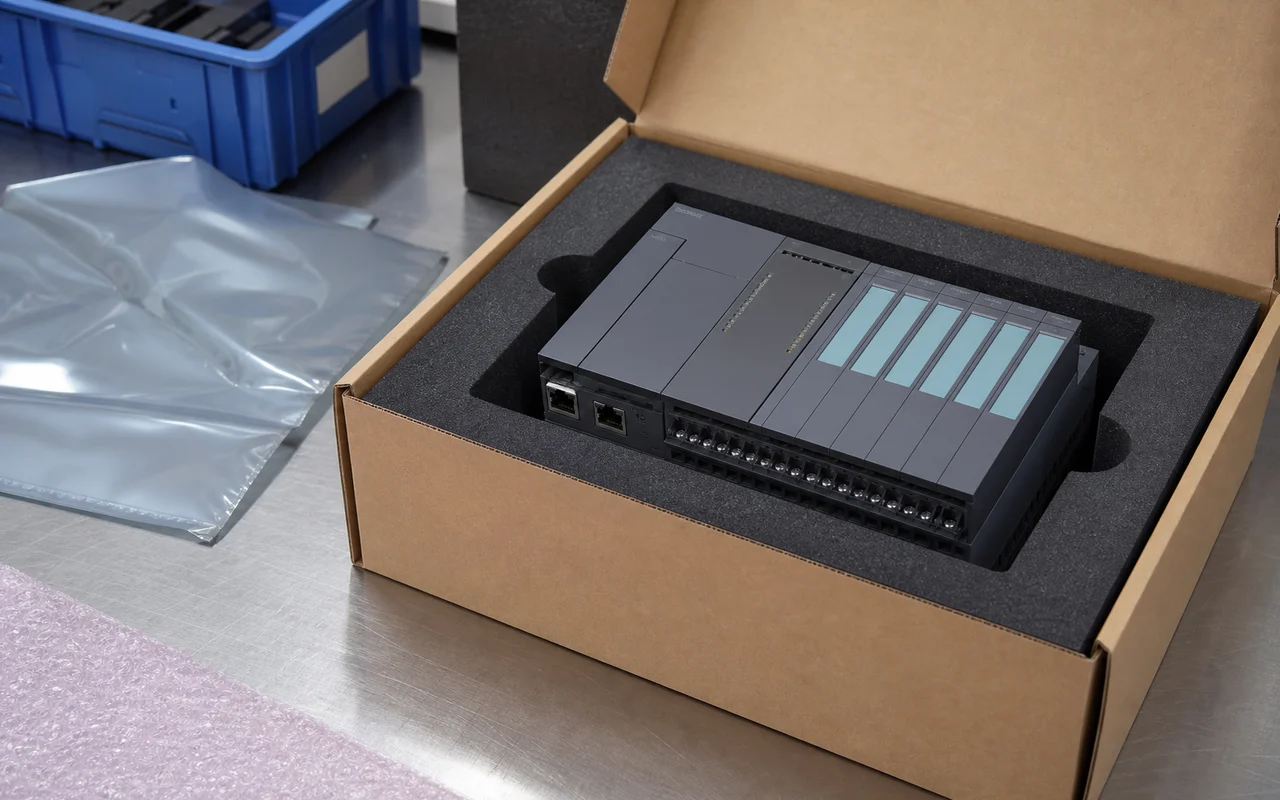 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.