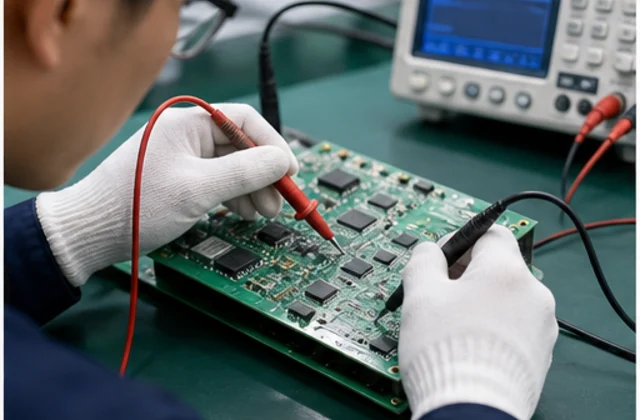
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
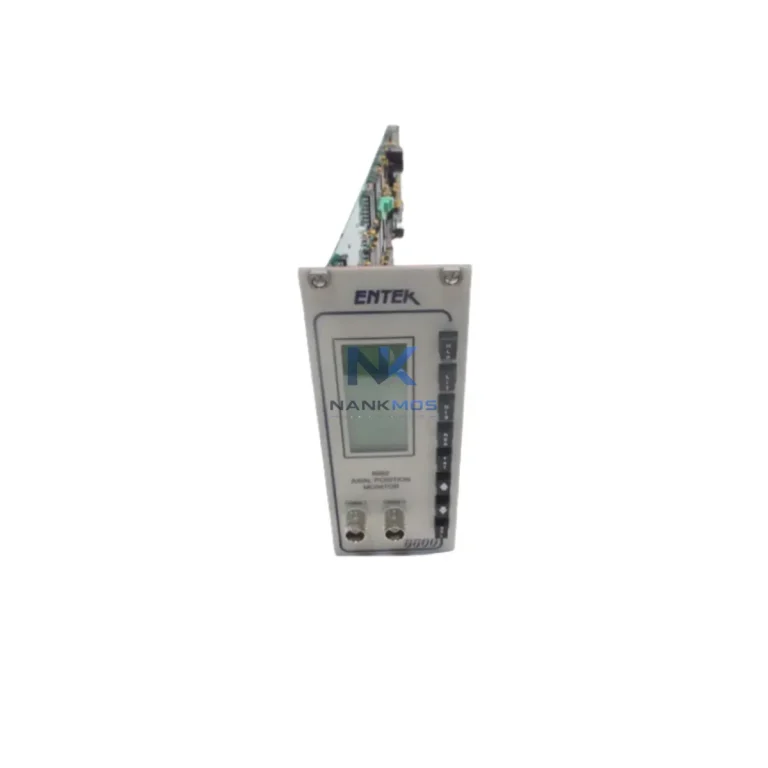
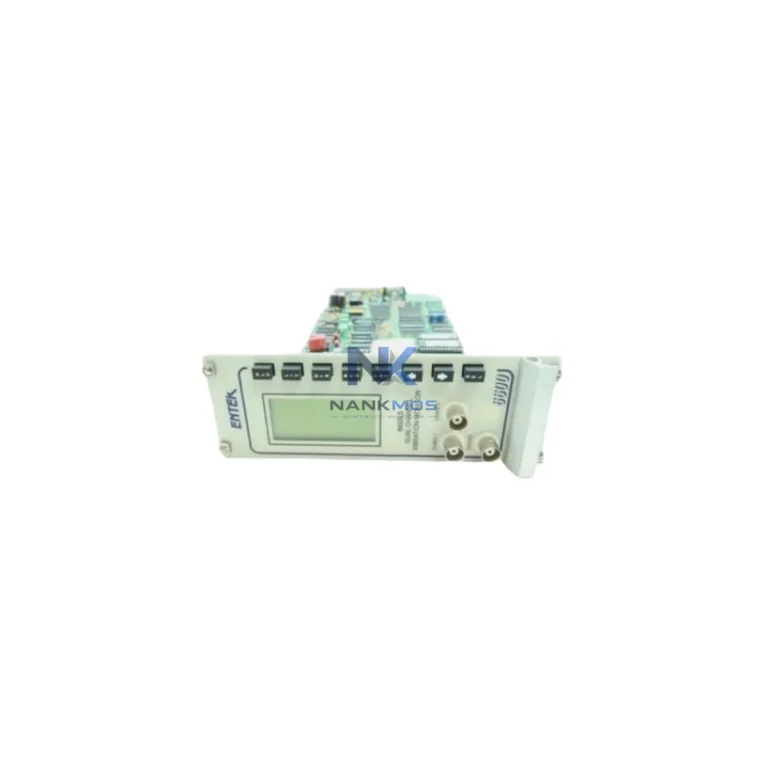
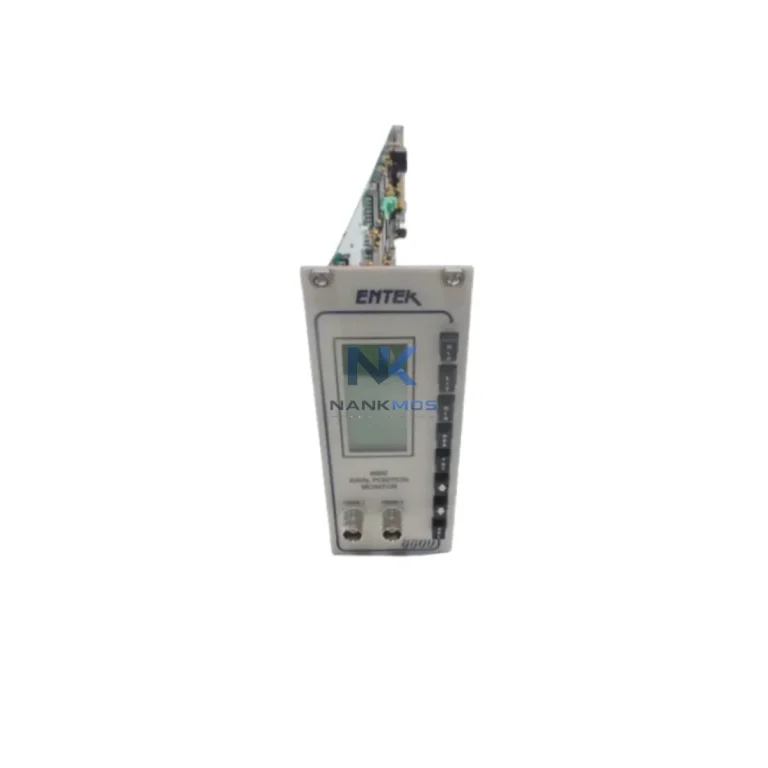
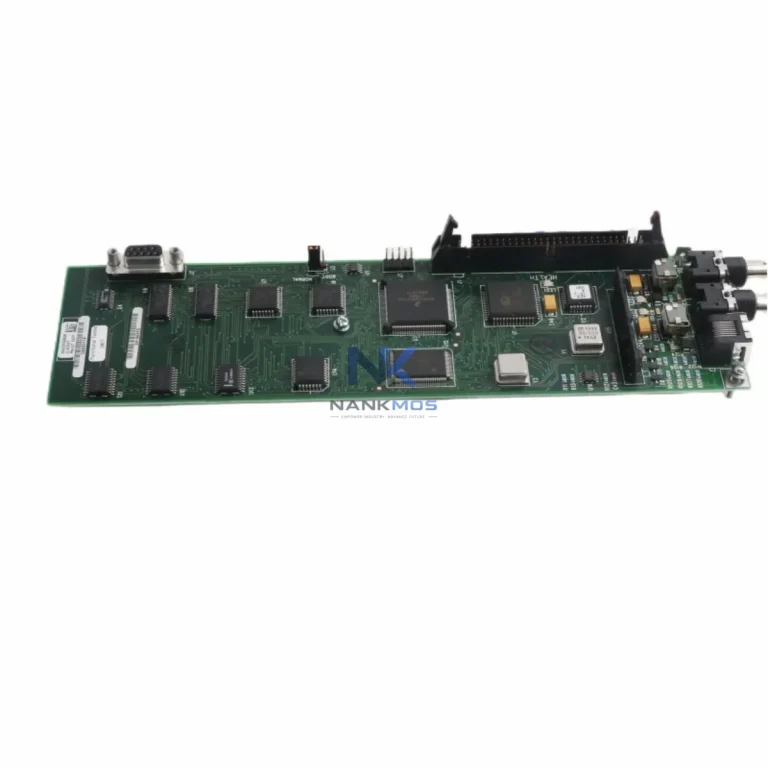
Entek 6652 EC6652 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.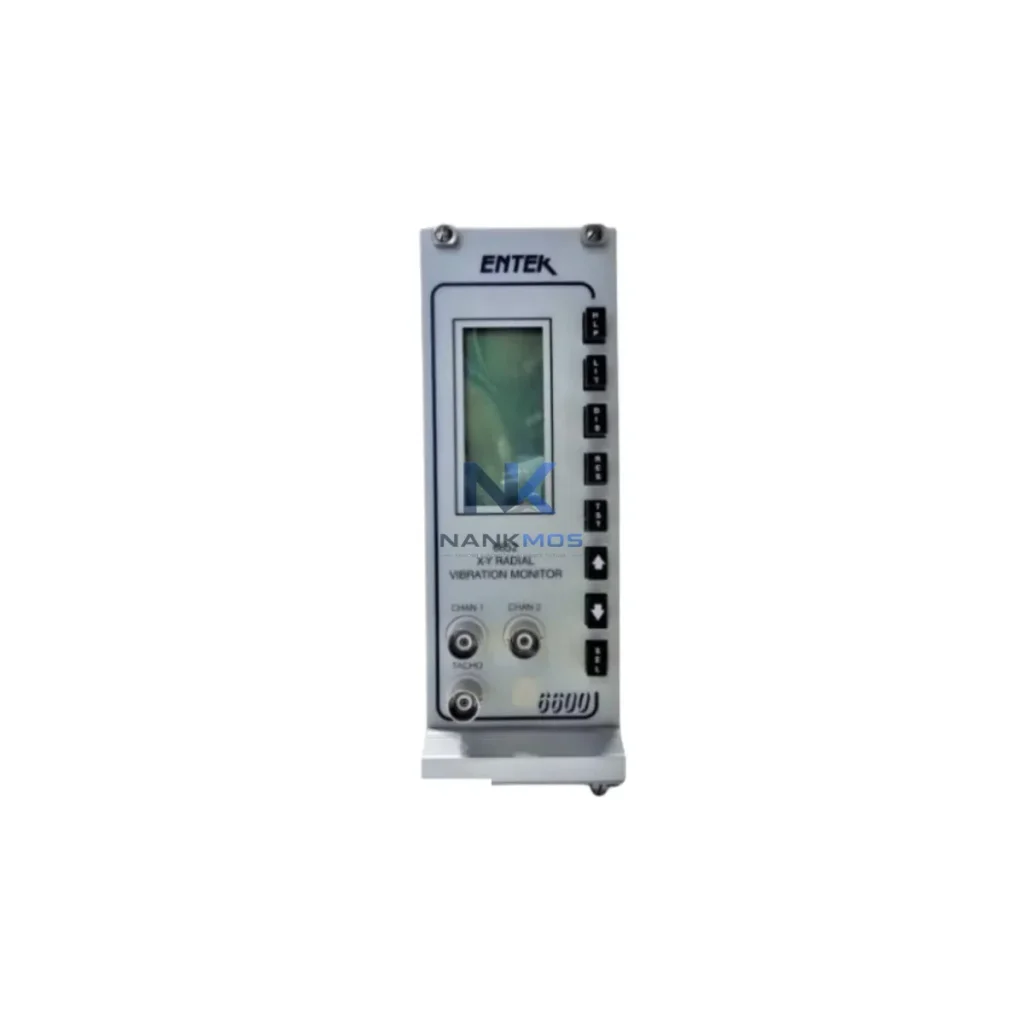
Entek 6652 EC6652 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | Entek |
|---|---|
| Application | Turbine & Condition Monitoring |
| Part Number / Model | 6652 EC6652 |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Monitoring Module |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The ENTEK EC6652 Radial Vibration Monitor is a precision sensing and signal-conditioning module engineered for the ENTEK 6652 Series continuous machinery protection platform. Designed to operate at the intersection of field-level sensing and plant-wide data infrastructure, the EC6652 delivers real-time radial vibration data across the full automation stack — from rotating equipment and proximity probes through PLC controllers, remote I/O nodes, HMI panels, SCADA systems, and edge gateways — enabling a seamless, uninterrupted data chain across the smart factory floor.
In modern industrial environments, vibration data is no longer siloed at the machine level. The EC6652 integrates directly into the ENTEK 6652 rack-based monitoring architecture, where it works alongside companion modules such as the ENTEK EC6600 Keyphasor Module and ENTEK EC6620 Thrust Position Monitor to form a complete machinery health monitoring node. This node feeds structured, time-stamped vibration amplitude and phase data upstream to distributed control systems and condition monitoring software, supporting predictive maintenance workflows and reducing unplanned downtime across compressors, turbines, pumps, and rotating machinery assets.
The EC6652's role in the smart factory data chain begins at the machine shaft. Eddy-current proximity probes mounted on rotating equipment — compressors, steam turbines, centrifugal pumps — feed continuous displacement signals into the EC6652 module seated in the ENTEK 6652 rack chassis. The module conditions, scales, and evaluates these signals against configurable Alert and Danger thresholds, triggering relay outputs for immediate machine protection while simultaneously passing processed vibration data across the rack backplane.
At the rack level, the EC6652 operates in coordination with the ENTEK EC6600 Keyphasor Module, which provides shaft reference pulses for phase and speed calculations, and the ENTEK EC6621 Axial Position Monitor, which tracks thrust bearing displacement. Together, these modules create a multi-parameter machinery health dataset that is aggregated by the rack's communication interface and forwarded to upstream systems.
For protocol conversion and network integration, the 6652 rack output is typically bridged through an industrial protocol gateway — such as a Moxa MGate or ProSoft MVI series — that translates proprietary rack data into Modbus TCP/IP or OPC-UA, making it consumable by plant-level SCADA platforms including GE iFIX, Wonderware System Platform, or Rockwell FactoryTalk. This gateway layer is critical in multi-vendor environments where Allen-Bradley ControlLogix PLCs or Siemens S7-300/S7-400 controllers serve as the primary automation backbone but lack native ENTEK protocol support.
From the SCADA layer, vibration trend data from the EC6652 is visualized on HMI panels — such as Rockwell PanelView Plus or Siemens SIMATIC HMI — where operators monitor real-time shaft displacement, vibration amplitude, and alarm status. Simultaneously, the data stream is archived in historian databases for long-term trend analysis, enabling maintenance engineers to identify developing faults — bearing wear, rotor imbalance, misalignment — weeks before they escalate to unplanned shutdowns.
For remote diagnostics, the EC6652 data path extends through edge computing gateways — such as Advantech WISE-5000 series or Moxa UC-8100 — which aggregate multi-point vibration data from multiple 6652 racks across a plant, apply edge analytics, and push summarized health indices to cloud-based condition monitoring dashboards or enterprise asset management (EAM) systems. This architecture supports remote engineering teams in diagnosing vibration anomalies without requiring on-site access, reducing travel costs and accelerating fault response times.
The complete data chain — proximity probe → EC6652 module → rack backplane → protocol gateway → PLC/DCS → SCADA/HMI → edge gateway → cloud dashboard — represents the full smart factory connectivity loop that the ENTEK EC6652 anchors at the field sensing layer. Complementary components such as the ENTEK EC6640 Speed Monitor, ENTEK EC6650 Radial Vibration Monitor (single-channel variant), and rack power supply modules complete the 6652 Series ecosystem, ensuring that every critical rotating asset on the plant floor is continuously monitored, networked, and visible to operations and maintenance teams in real time.
Many industrial facilities operate with fragmented monitoring architectures — legacy vibration monitors that generate local alarms but cannot transmit structured data to SCADA or DCS platforms, creating data islands that prevent plant-wide visibility. The ENTEK EC6652, deployed within the 6652 Series rack system, directly addresses these gaps:
Protocol Fragmentation: Where plant networks run Modbus TCP, PROFIBUS, or OPC-UA but the monitoring rack uses proprietary backplane communication, a protocol gateway bridges the EC6652 data into the plant network without requiring custom software development or controller reprogramming.
Data Islands and Siloed Monitoring: By integrating the EC6652 into a networked rack architecture connected to SCADA, all vibration data from multiple machines is centralized into a single historian and visualization layer, eliminating the need for manual data collection rounds and paper-based maintenance logs.
Remote Monitoring Gaps: In facilities where maintenance engineers are not permanently on-site, the EC6652's alarm relay outputs — combined with edge gateway connectivity — enable remote alarm notification via email, SMS, or SCADA push alerts, ensuring that developing faults are flagged immediately regardless of personnel location.
Production Line Transparency: Real-time vibration data from the EC6652 feeds into OEE (Overall Equipment Effectiveness) dashboards, giving production managers visibility into machinery health as a factor in line availability, supporting data-driven maintenance scheduling and reducing reactive maintenance costs.
System Scalability: The modular 6652 rack architecture allows additional EC6652 channels, thrust position monitors, and speed monitors to be added as monitoring scope expands, without replacing the existing communication infrastructure or SCADA configuration.
Q1: Can the ENTEK EC6652 integrate with Modbus TCP/IP or OPC-UA SCADA systems? The EC6652 communicates via the ENTEK 6652 rack backplane. Integration with Modbus TCP/IP or OPC-UA SCADA platforms is achieved through an industrial protocol gateway (e.g., Moxa MGate, ProSoft MVI) that translates rack data into standard industrial protocols. This approach is widely deployed in GE, Rockwell, and Siemens SCADA environments without requiring modifications to the EC6652 module itself.
Q2: What is the communication latency for alarm relay outputs on the EC6652? The EC6652 evaluates vibration signals continuously and triggers Alert and Danger relay outputs in real time, with response times consistent with hardware relay switching — typically within milliseconds of threshold crossing. This ensures that machine protection actions (trip signals, shutdown commands) are executed without communication network latency affecting safety response.
Q3: Is the ENTEK EC6652 compatible with multi-vendor automation environments? Yes. The 6652 Series rack architecture is designed as a standalone machinery protection system that interfaces with any PLC, DCS, or SCADA platform via analog outputs, relay contacts, and protocol gateways. It operates independently of the plant automation controller brand, making it compatible with Allen-Bradley, Siemens, ABB, Honeywell, and Emerson DeltaV environments.
Q4: What warranty and pre-shipment testing does NANKMOS provide for the EC6652? All ENTEK EC6652 units supplied by NANKMOS carry a 12-month warranty from the date of shipment. Each unit undergoes pre-shipment functional testing to verify signal conditioning, alarm relay operation, and backplane communication integrity before dispatch. In-stock inventory ensures rapid order fulfillment for maintenance and replacement requirements globally.
Functional Inspection100% tested on professional platforms to ensure stable performance.
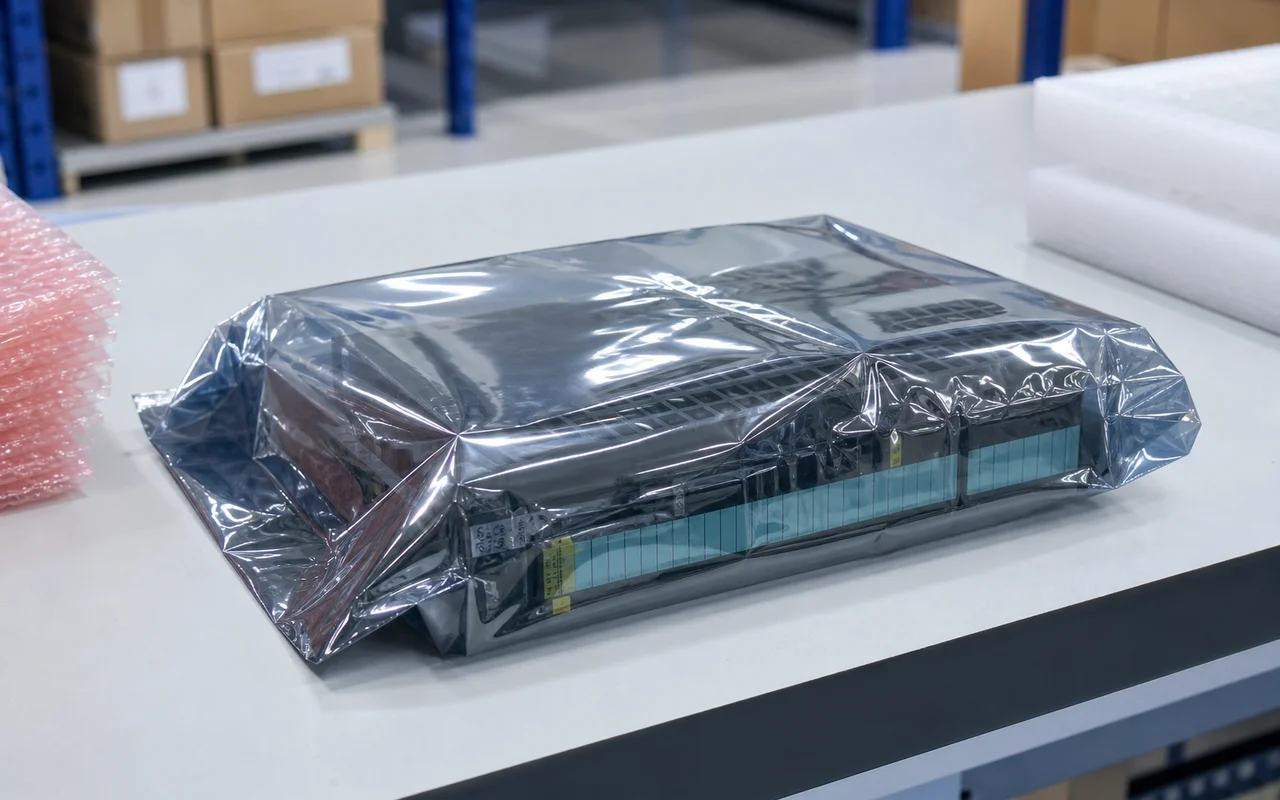 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
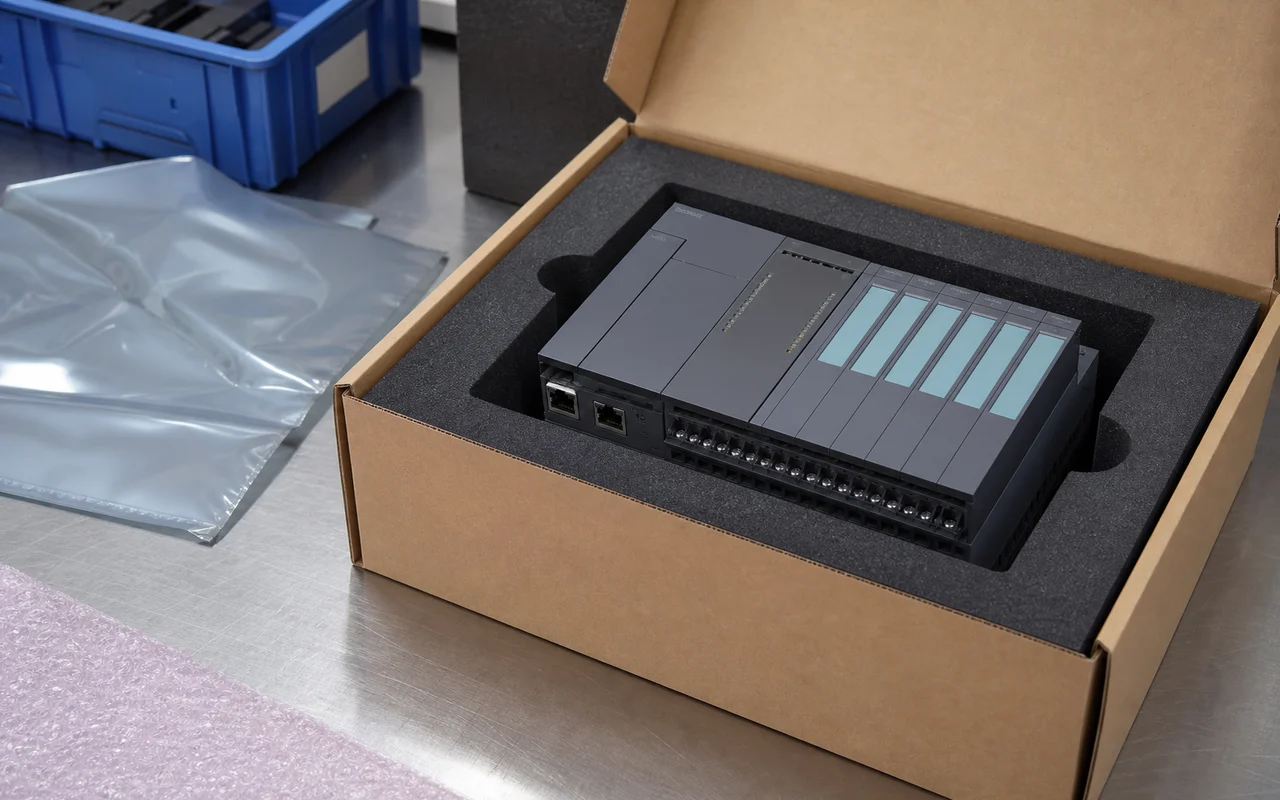 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.