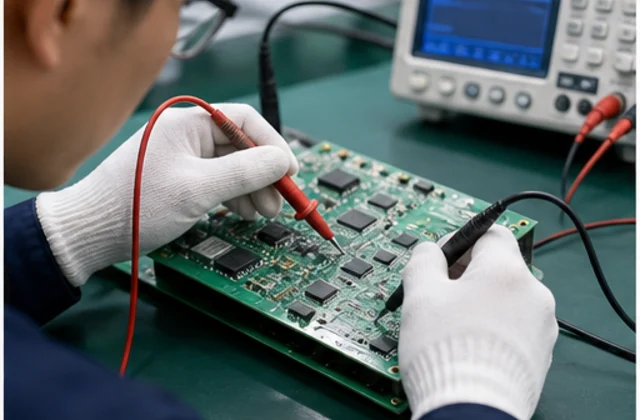
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
ROTORK IQT MOD6G is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.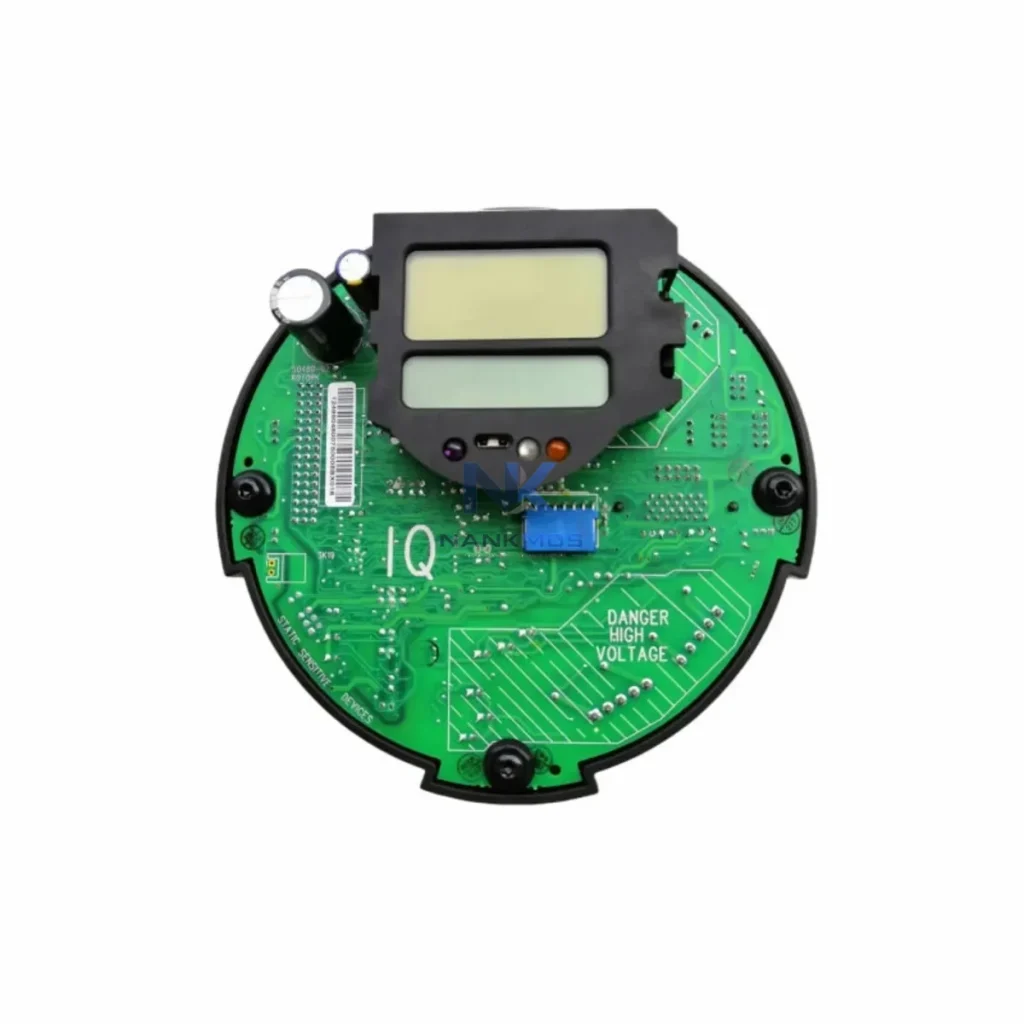
ROTORK IQT MOD6G is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | ROTORK |
|---|---|
| Application | Industrial Network Communication |
| Part Number / Model | IQT MOD6G |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Communication Module |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
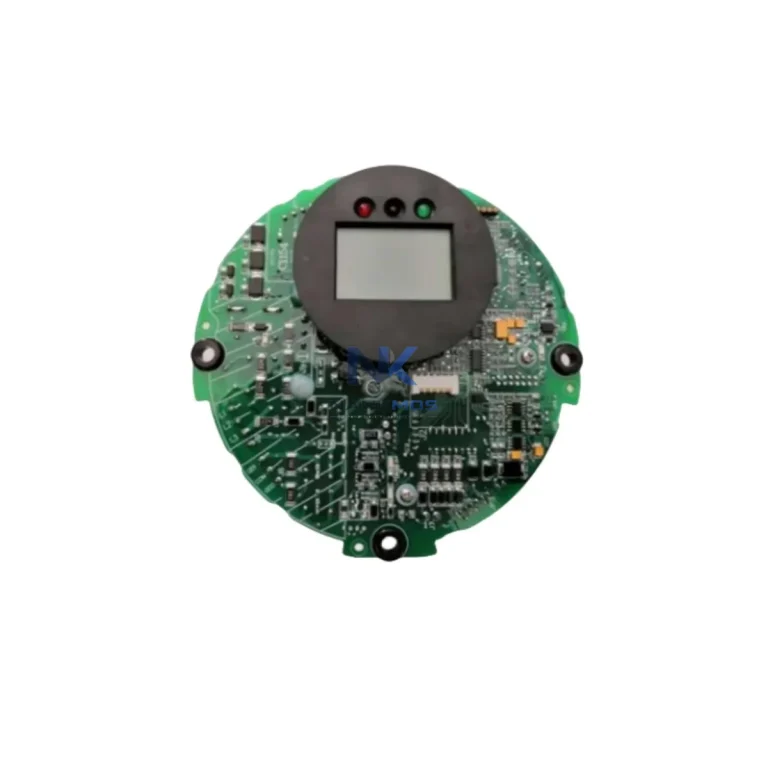
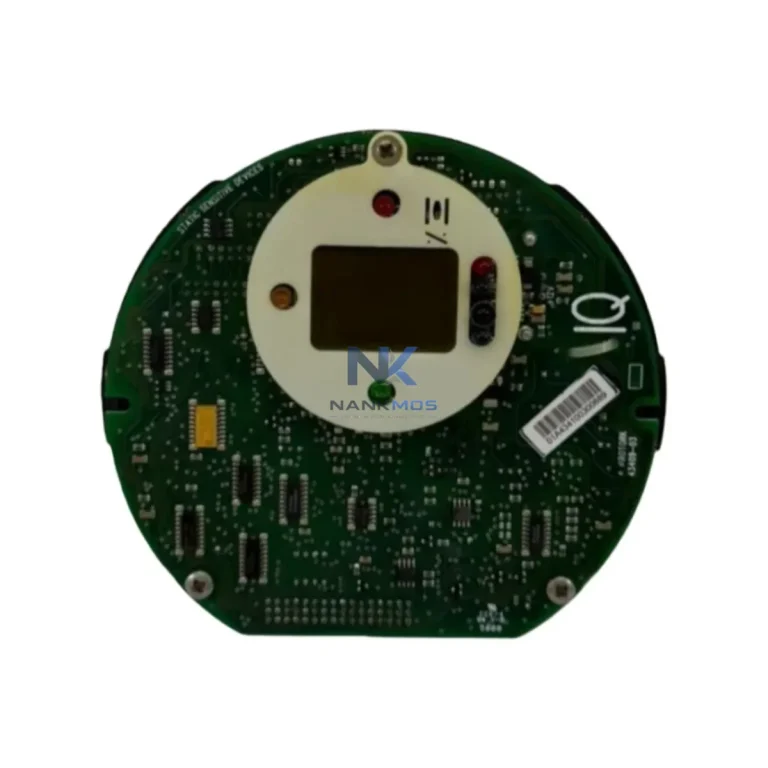
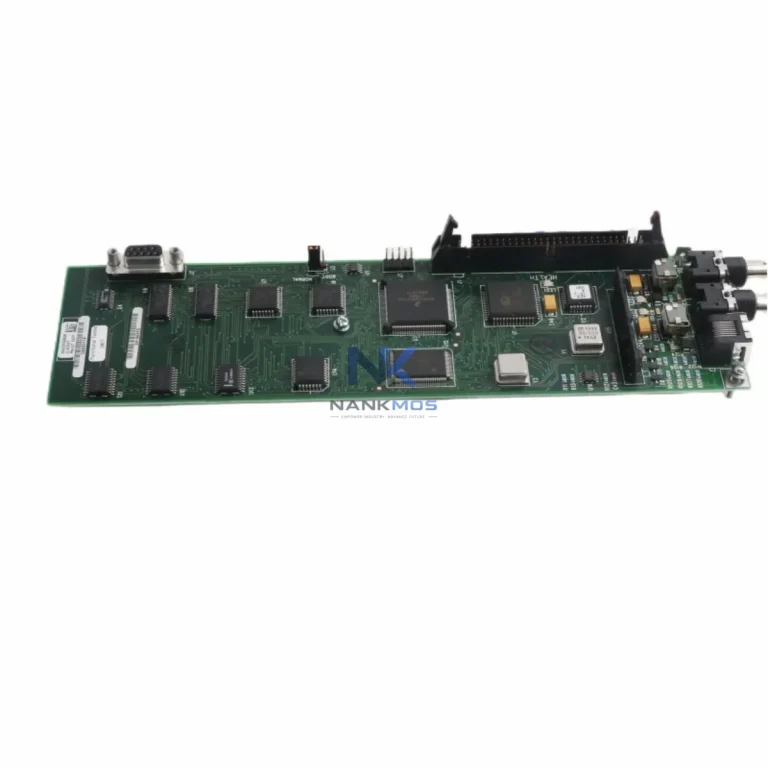
The Rotork IQT-MOD6G is a precision-engineered industrial protocol gateway and network interface module designed specifically for the Rotork IQ Series electric actuator platform. In modern smart factory environments where seamless data flow between field devices, control systems, and supervisory platforms is non-negotiable, the IQT-MOD6G serves as the critical communication bridge that eliminates data silos and enables full actuator visibility across the automation stack.
Deployed at the intersection of field instrumentation and plant-level control, the IQT-MOD6G translates native actuator signals into standardized industrial protocols — enabling upstream systems such as Siemens S7-1500 PLCs, Rockwell ControlLogix controllers, and Yokogawa CENTUM VP DCS platforms to receive real-time valve position, torque feedback, fault status, and operational diagnostics without custom engineering overhead. This plug-and-play protocol conversion capability dramatically reduces commissioning time and integration risk on greenfield and brownfield automation projects alike.
In a fully integrated smart factory architecture, the IQT-MOD6G sits at the field layer, mounted directly on Rotork IQ Series or IQT Series electric actuators controlling critical process valves in pipelines, chemical dosing systems, water treatment plants, and energy distribution networks. From this position, it continuously captures actuator telemetry — including valve open/close position, motor torque curves, thermal status, and fault event logs — and transmits this data upstream via Modbus RTU over RS-485 or Modbus TCP over Industrial Ethernet.
At the control layer, a Siemens S7-300 or S7-1500 PLC receives structured Modbus register data from multiple IQT-MOD6G nodes simultaneously, enabling coordinated valve sequencing, interlock logic, and process safety functions. In parallel, a Rockwell Automation ControlLogix L8x controller may handle high-speed loop control while the IQT-MOD6G feeds actuator health data into the EtherNet/IP network segment via a protocol bridge.
For remote I/O expansion, the IQT-MOD6G integrates naturally with Wago 750-series Modbus I/O modules and Phoenix Contact Axioline F remote I/O stations, allowing distributed actuator nodes across large plant footprints to be aggregated into a single Modbus master scan cycle. This eliminates the need for dedicated hardwired signal runs between field actuators and the control room, reducing cable costs and improving system scalability.
At the supervisory layer, Wonderware InTouch HMI and Ignition SCADA by Inductive Automation platforms connect directly to the Modbus TCP network, pulling live actuator data for real-time process visualization, trend logging, and alarm management. Operators gain instant visibility into valve positions across an entire facility — from a single control room workstation or a mobile tablet interface — without requiring additional OPC-UA middleware when the IQT-MOD6G's native Modbus TCP output is used.
For HART-enabled installations, the IQT-MOD6G's secondary HART channel allows integration with Emerson AMS Device Manager and ABB Asset Vision asset management platforms, enabling predictive maintenance workflows based on actuator wear data, torque signature analysis, and historical fault trending. This HART pathway also supports integration with Pepperl+Fuchs FieldConnex HART multiplexers for high-density multi-drop actuator networks in petrochemical and refinery environments.
Edge computing nodes — such as the Moxa UC-8112 industrial computer or Advantech WISE-5000 edge gateway — can be deployed alongside the IQT-MOD6G to perform local data preprocessing, protocol normalization, and secure MQTT/OPC-UA uplink to cloud-based MES or ERP platforms. This edge-to-cloud architecture ensures that actuator data contributes to plant-wide OEE calculations, energy consumption analytics, and digital twin models without burdening the core PLC network with additional polling overhead.
Many industrial facilities operate with legacy actuator fleets that lack native digital communication capability, creating persistent data gaps between field devices and plant control systems. The IQT-MOD6G directly addresses this challenge by providing a standardized Modbus interface that integrates seamlessly with existing PLC and SCADA infrastructure — no proprietary software, no custom drivers, no extended commissioning cycles.
Protocol fragmentation is one of the most common barriers to smart factory transformation. Sites running mixed fleets of Modbus RTU, HART, and proprietary serial devices struggle to consolidate data into a unified supervisory view. The IQT-MOD6G resolves this by acting as a multi-protocol gateway, normalizing actuator data into Modbus register maps that any standard SCADA or DCS platform can consume directly.
Data island elimination is achieved by connecting previously isolated actuator nodes into the plant Ethernet backbone. Valve positions, torque readings, and fault codes that were previously only accessible via local LCD display or handheld communicator are now available in real time on the SCADA dashboard, enabling faster operator response to process deviations and reducing unplanned downtime.
Remote monitoring and diagnostics become fully operational once the IQT-MOD6G is commissioned. Maintenance engineers can interrogate actuator health parameters — motor temperature, number of operations, torque switch settings, and battery backup status — from the control room or via VPN-connected remote access terminals, eliminating the need for physical site visits to remote or hazardous locations.
Production line transparency is enhanced through continuous actuator status reporting to the SCADA historian. Trend data captured over weeks and months enables engineering teams to identify valve cycling patterns, detect early signs of mechanical wear, and schedule preventive maintenance during planned shutdowns rather than reacting to unexpected failures.
Alarm management and traceability are strengthened by the IQT-MOD6G's ability to timestamp and transmit fault events — including torque trip, thermal overload, and loss of phase — directly to the SCADA alarm server. This creates a complete, auditable event log that supports root cause analysis, regulatory compliance reporting, and insurance documentation.
System scalability is a core design principle of the IQT-MOD6G architecture. As plant capacity expands, additional actuator nodes can be added to the Modbus RS-485 network (up to 247 devices per segment) or the Ethernet backbone without requiring changes to the master PLC program or SCADA configuration — only new Modbus register address assignments are needed.
All units supplied by NANKMOS are sourced from authorized distribution channels, undergo pre-shipment functional verification, and are backed by a 12-month warranty covering manufacturing defects and communication interface failures. Inventory is maintained in-stock for rapid dispatch to support urgent project timelines and MRO replacement requirements.
Q1: What is the maximum Modbus polling rate supported by the IQT-MOD6G, and will high-frequency polling cause communication latency?The IQT-MOD6G supports Modbus RTU at baud rates up to 115,200 bps and Modbus TCP at 10/100 Mbps Ethernet speeds. For typical actuator monitoring applications with 1–5 second scan cycles, communication latency is negligible. For high-density networks with 50+ actuator nodes, it is recommended to segment the RS-485 bus into multiple Modbus master channels or use Modbus TCP for lower latency and higher throughput.
Q2: Is the IQT-MOD6G compatible with third-party SCADA platforms beyond Rotork's own software?Yes. Because the IQT-MOD6G uses standard Modbus RTU and Modbus TCP protocols, it is fully compatible with any SCADA, DCS, or HMI platform that supports Modbus — including Ignition, Wonderware, iFIX, Citect, and WinCC. No proprietary drivers or Rotork-specific software licenses are required for basic integration. HART secondary channel integration may require an asset management platform with HART pass-through capability.
Q3: How does the IQT-MOD6G support remote diagnostics in hazardous or hard-to-access locations?Once connected to the plant Modbus TCP network, the IQT-MOD6G continuously transmits actuator diagnostic registers — including torque profile, thermal status, operation counter, and fault history — to the SCADA historian. Maintenance teams can access this data remotely via the SCADA client or a secure VPN connection, enabling condition-based maintenance decisions without physical access to the actuator. This is particularly valuable for actuators installed in elevated, confined, or classified hazardous area locations.
Q4: What warranty coverage is provided, and what does the pre-shipment test include?All IQT-MOD6G units supplied by NANKMOS carry a 12-month warranty from the date of shipment, covering manufacturing defects and communication interface failures under normal operating conditions. Pre-shipment testing includes Modbus RTU/TCP communication verification, HART channel continuity check, power supply input range validation, and visual inspection for physical integrity. Units failing any test criterion are quarantined and not dispatched. Replacement or repair is provided at no charge within the warranty period for confirmed manufacturing defects.
Functional Inspection100% tested on professional platforms to ensure stable performance.
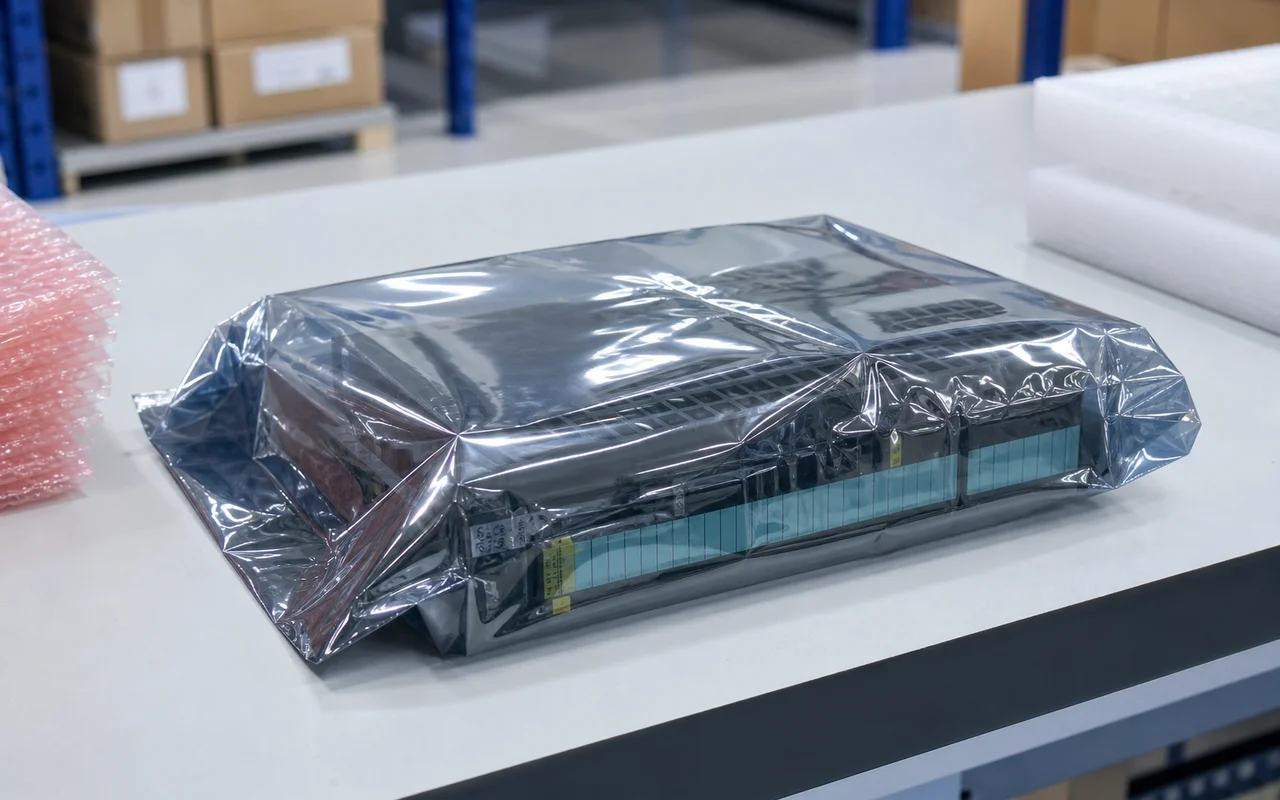 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
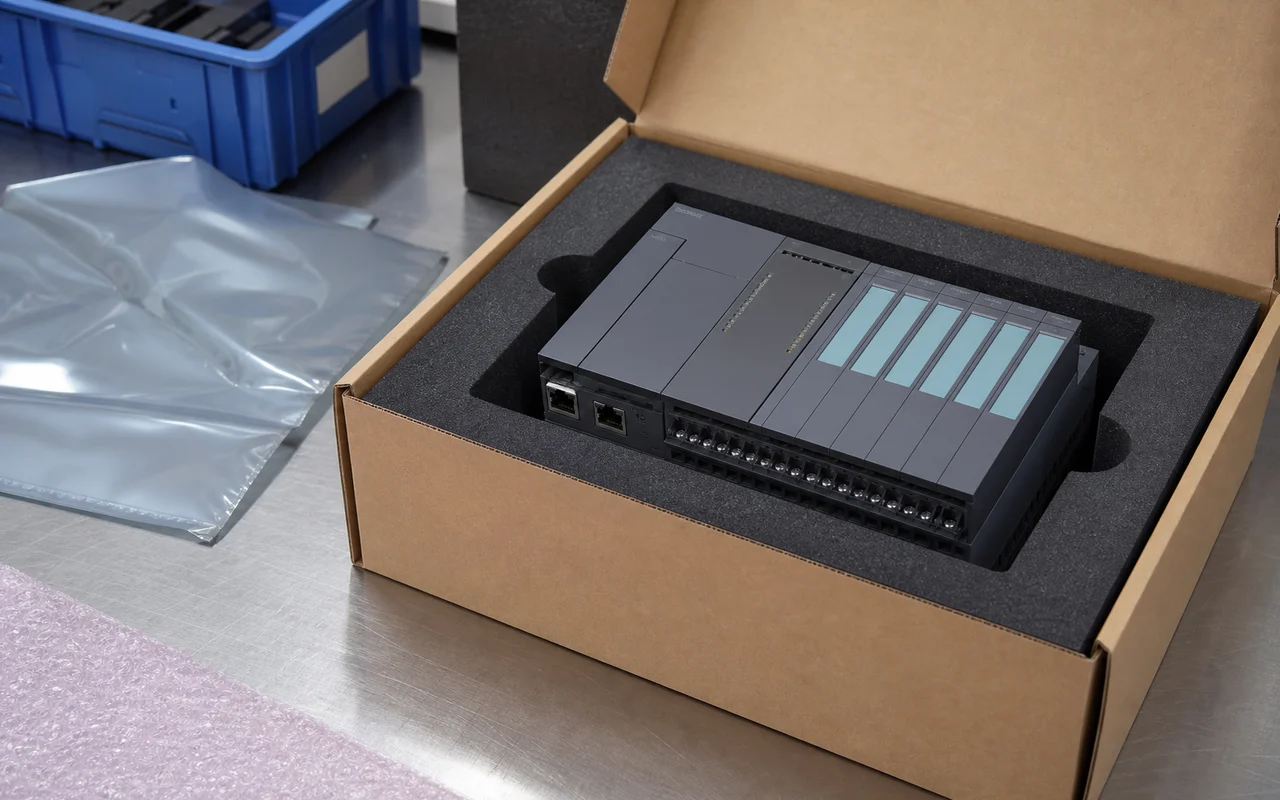 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.