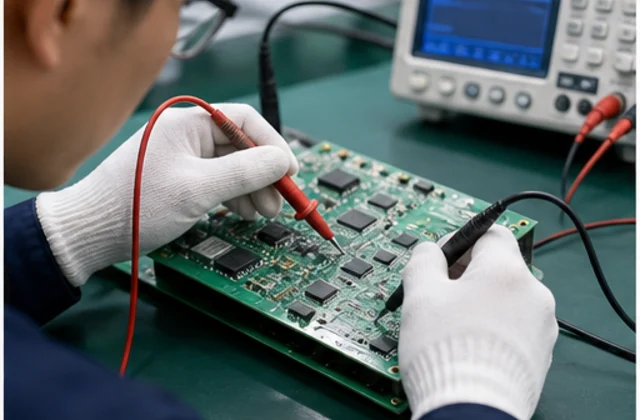
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
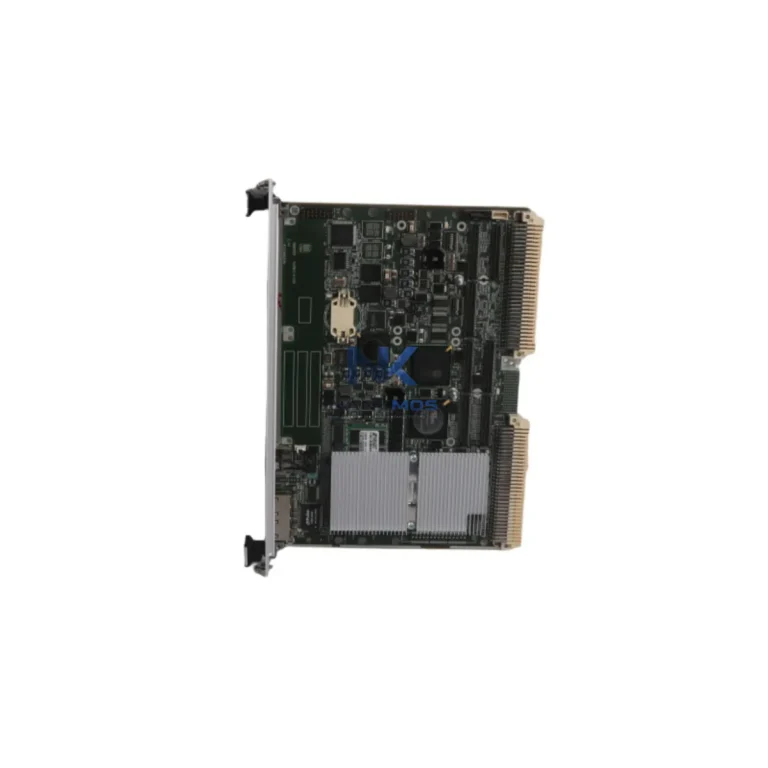
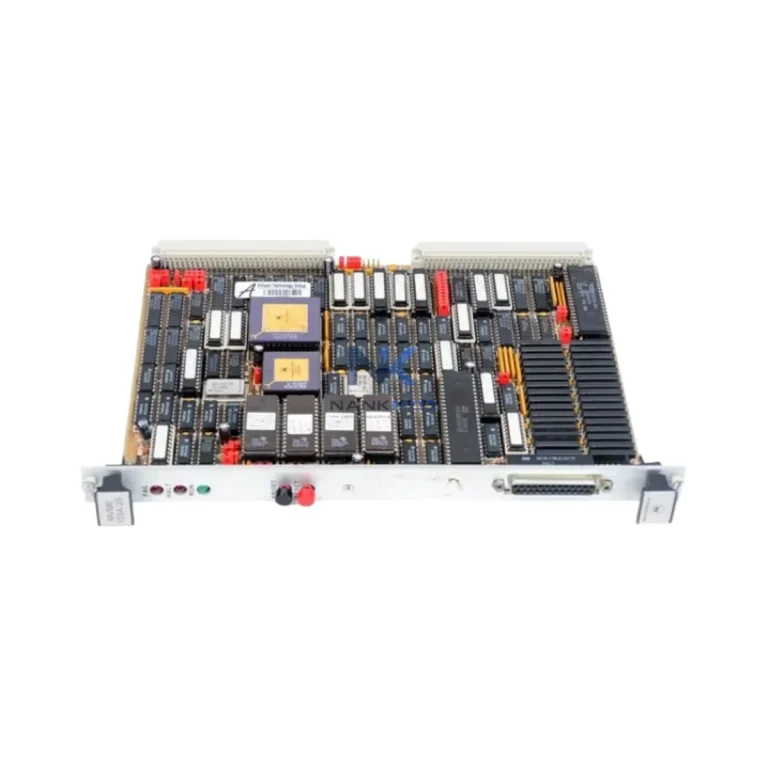
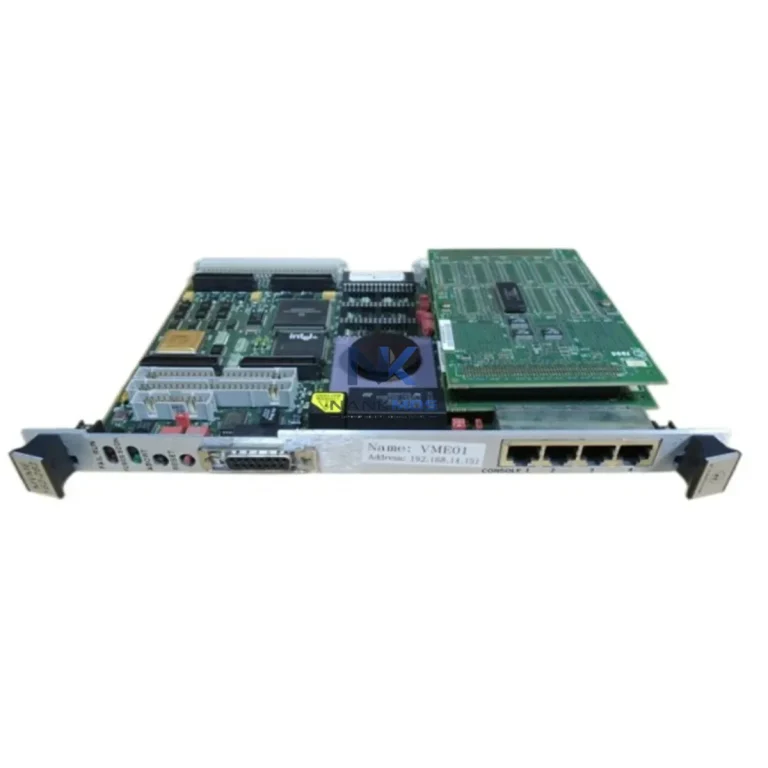
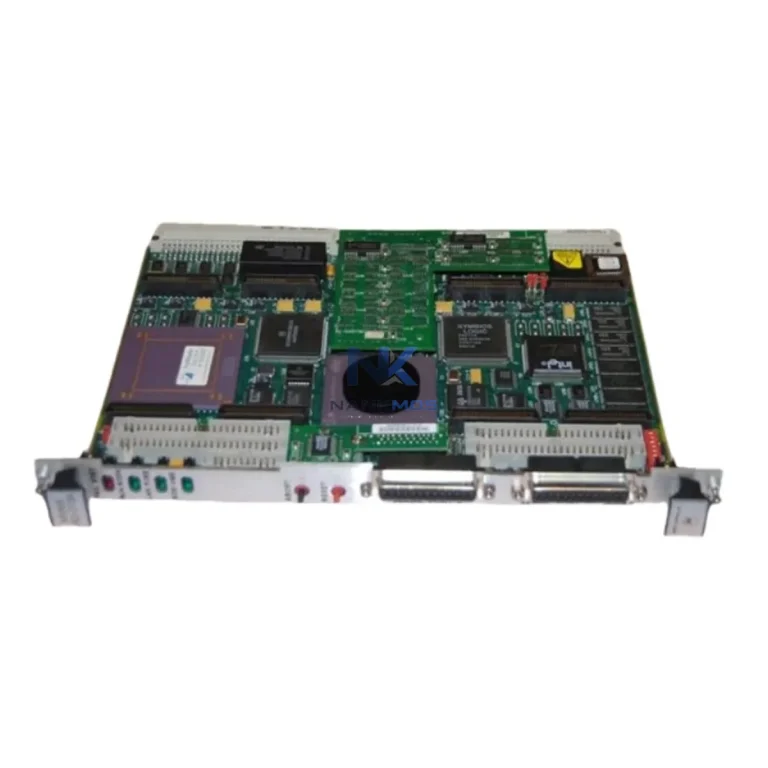
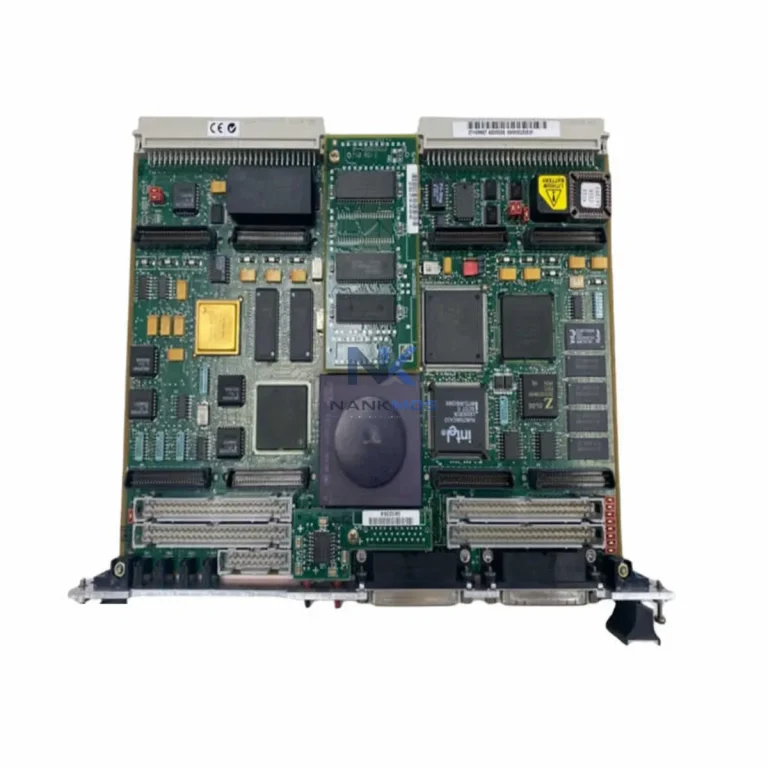
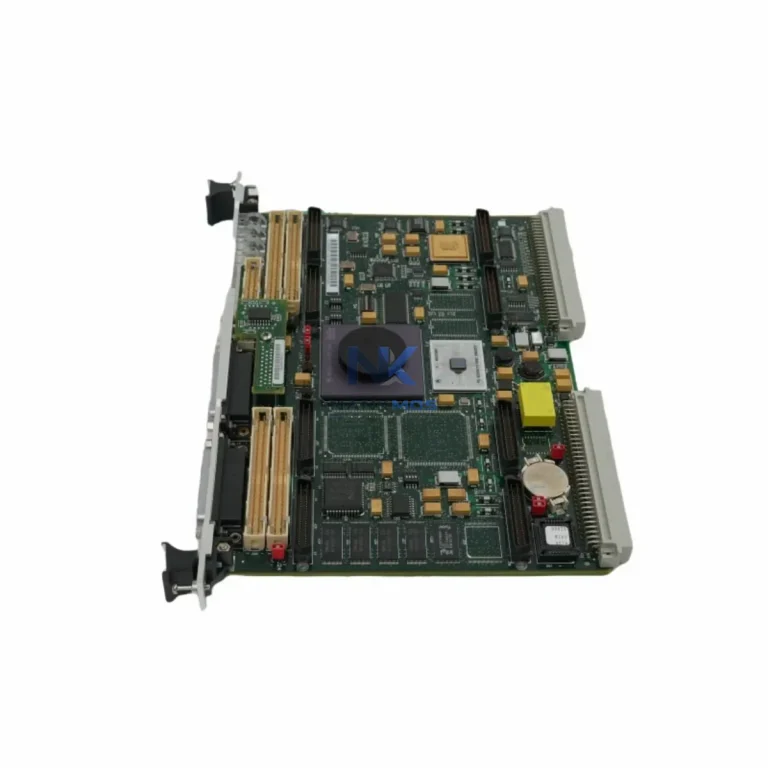
Motorola VME172PA 652SE is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.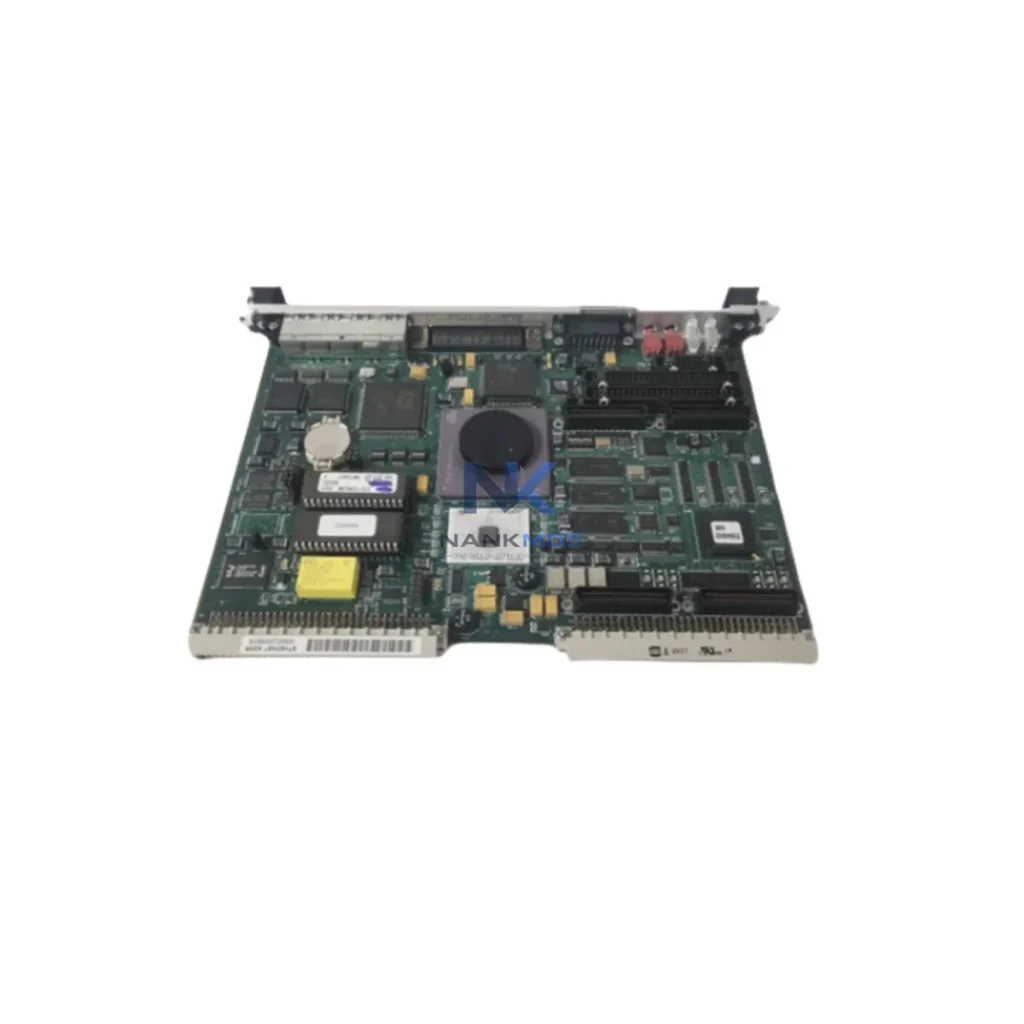
Motorola VME172PA 652SE is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | Motorola |
|---|---|
| Application | DCS / Control Board Replacement |
| Part Number / Model | VME172PA 652SE |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Control Board / Card |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The Motorola VME172PA-652SE is a high-performance VMEbus Single Board Computer (SBC) built on the PowerPC architecture, engineered to serve as a robust network-linked processing node within demanding industrial automation environments. Designed for seamless integration across VME-based control platforms, this SBC bridges the gap between legacy field devices and modern smart factory data infrastructure — enabling real-time data acquisition, protocol conversion, and deterministic communication across multi-tier industrial networks.
In today's connected manufacturing landscape, the ability to move data reliably from field-level sensors and actuators through PLC controllers, remote I/O modules, HMI terminals, SCADA systems, and up to enterprise MES/ERP platforms is non-negotiable. The VME172PA-652SE is purpose-built to anchor this data flow, providing the computational backbone for intelligent edge processing, alarm management, and remote diagnostics within VME-based automation architectures.
The VME172PA-652SE operates at the heart of a layered industrial data architecture. At the field level, sensors — including pressure transmitters, temperature probes, and proximity switches — feed raw process data into remote I/O modules such as the Motorola MVME162 or compatible VME I/O carrier boards. These signals are aggregated and passed via the VMEbus backplane to the VME172PA-652SE, which executes real-time data processing and protocol normalization.
Within the control tier, the VME172PA-652SE acts as a co-processor or primary controller alongside Motorola MVME5500 or MVME6100 series SBCs in multi-slot VME chassis configurations. Its Ethernet interface enables direct communication with Siemens S7-300/S7-400 PLCs via Modbus TCP or OPC DA/UA bridges, ensuring that process variables are continuously synchronized between the VME platform and the broader PLC network without data latency.
For HMI and SCADA integration, the VME172PA-652SE connects to Wonderware InTouch or Ignition SCADA servers over industrial Ethernet, delivering live tag data for operator visualization, trend logging, and alarm management. Industrial managed switches — such as those from the Hirschmann MACH or Cisco IE 2000 series — provide the network backbone, ensuring redundant ring topologies (RSTP/MRP) that maintain uptime even during link failures.
At the edge, the VME172PA-652SE can interface with Moxa MGate or Advantech EKI series protocol gateways to bridge legacy serial field devices (RS-232/RS-485 Modbus RTU) into the Ethernet-based SCADA network. Variable frequency drives (VFDs) such as the ABB ACS880 or Siemens SINAMICS G120 — connected via Profibus DP or Modbus RTU — have their speed, torque, and fault data routed through the VME172PA-652SE for centralized monitoring and remote parameter adjustment.
Data visualization is achieved through integration with OSIsoft PI System or Kepware KEPServerEX OPC servers, which subscribe to real-time tags published by the VME172PA-652SE. This enables plant-wide dashboards, KPI tracking, and predictive maintenance analytics — transforming raw field signals into actionable intelligence for operations teams.
Remote diagnostics are supported via the SBC's Ethernet management port, allowing engineers to perform firmware updates, log retrieval, and system health checks without physical site access. Combined with SNMP-based network monitoring, the VME172PA-652SE provides full visibility into node status, communication errors, and CPU load — critical for minimizing unplanned downtime in 24/7 production environments.
Many industrial sites operating VME-based control systems face persistent challenges: protocol fragmentation between legacy serial devices and modern Ethernet networks, data silos that prevent SCADA systems from accessing field-level diagnostics, and limited remote visibility into distributed control nodes. The VME172PA-652SE directly addresses these pain points.
Protocol Unification: By supporting both VMEbus backplane communication and standard TCP/IP Ethernet, the VME172PA-652SE eliminates the need for external protocol converters in many architectures. Serial Modbus RTU devices can be bridged to Modbus TCP through the SBC's onboard serial ports, consolidating protocol stacks and reducing network complexity.
Eliminating Data Silos: The SBC's multi-interface design ensures that data from VME I/O modules, serial field instruments, and Ethernet-connected PLCs is aggregated into a single processing node — making it available to SCADA, MES, and cloud analytics platforms simultaneously, without duplicating infrastructure.
Remote Monitoring and Alarm Tracking: With Ethernet connectivity and support for SNMP and OPC protocols, the VME172PA-652SE enables remote engineers to monitor system health, acknowledge alarms, and retrieve historical logs from any networked workstation. This reduces the need for on-site intervention and accelerates fault resolution.
Production Line Transparency: By serving as the data aggregation point for multiple VME I/O slots, the SBC provides a unified view of production line status — machine states, cycle counts, fault codes, and energy consumption — feeding this data upstream to SCADA dashboards and MES reporting modules.
Scalable System Expansion: The VMEbus architecture supports multi-board configurations, allowing additional I/O, communication, or processing modules to be added to the chassis as automation requirements grow — without redesigning the network topology or replacing the core SBC.
Q1: What communication protocols does the Motorola VME172PA-652SE support for SCADA and HMI integration?The VME172PA-652SE supports TCP/IP and UDP over its 10/100BaseT Ethernet interface, enabling Modbus TCP, OPC DA/UA, and SNMP communication with SCADA servers and HMI platforms. Its onboard serial ports support RS-232 and RS-422/RS-485 for legacy Modbus RTU and proprietary field device protocols, making it compatible with a wide range of industrial automation systems.
Q2: How does the VME172PA-652SE ensure network stability in 24/7 industrial environments?The SBC is designed for continuous industrial operation with a wide operating temperature range and robust VMEbus backplane connectivity. When deployed with managed industrial switches supporting RSTP or MRP ring redundancy, the network maintains communication continuity even during single-link failures. Pre-shipment functional testing ensures each unit is verified before dispatch.
Q3: Can the VME172PA-652SE be used for remote diagnostics and firmware management?Yes. The Ethernet management interface supports remote access for system diagnostics, log retrieval, and firmware updates. SNMP monitoring allows network management systems to track node health, communication error rates, and CPU utilization in real time — enabling proactive maintenance without requiring physical access to the VME chassis.
Q4: What warranty and supply assurance does NANKMOS provide for the VME172PA-652SE?NANKMOS provides a 12-month warranty on the Motorola VME172PA-652SE, backed by pre-shipment functional testing and in-stock inventory for rapid order fulfillment. Our supply chain supports urgent replacement requirements for production-critical VME systems, minimizing downtime risk for automation sites dependent on continuous operation.
Functional Inspection100% tested on professional platforms to ensure stable performance.
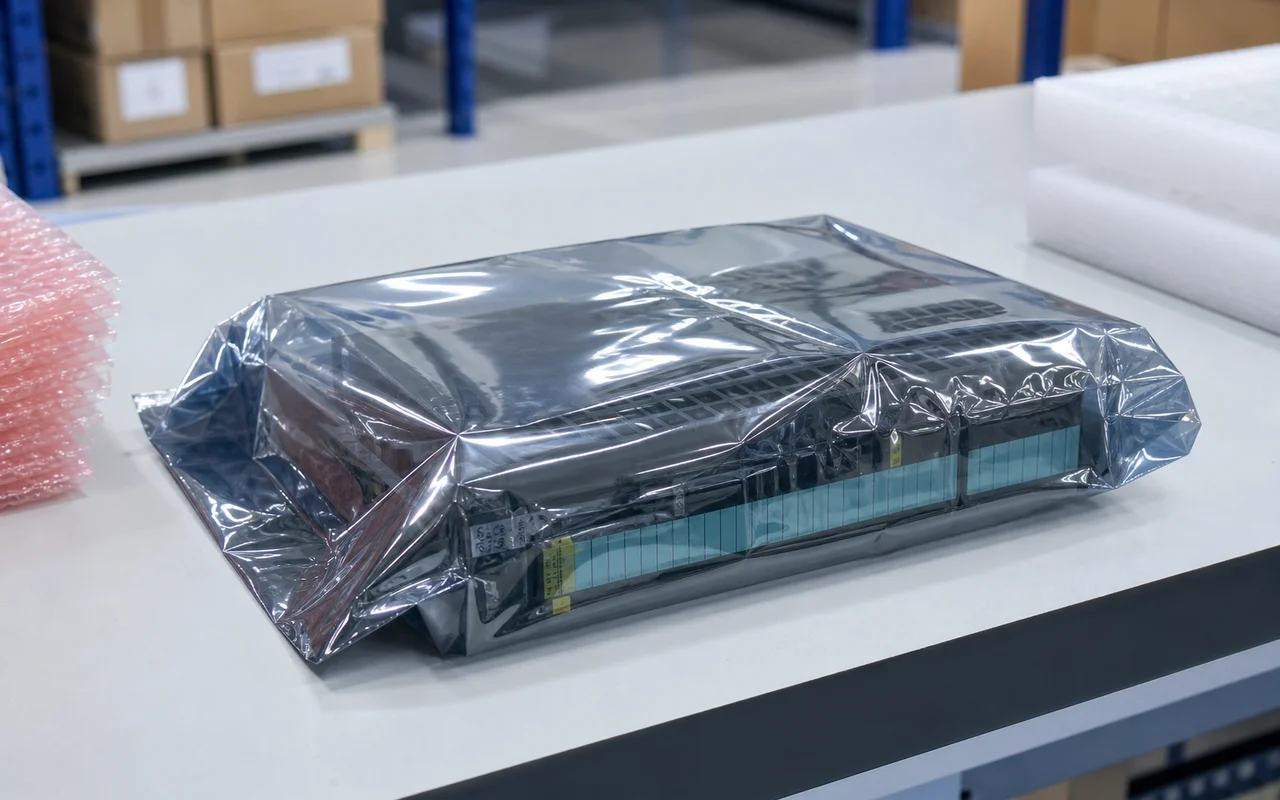 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
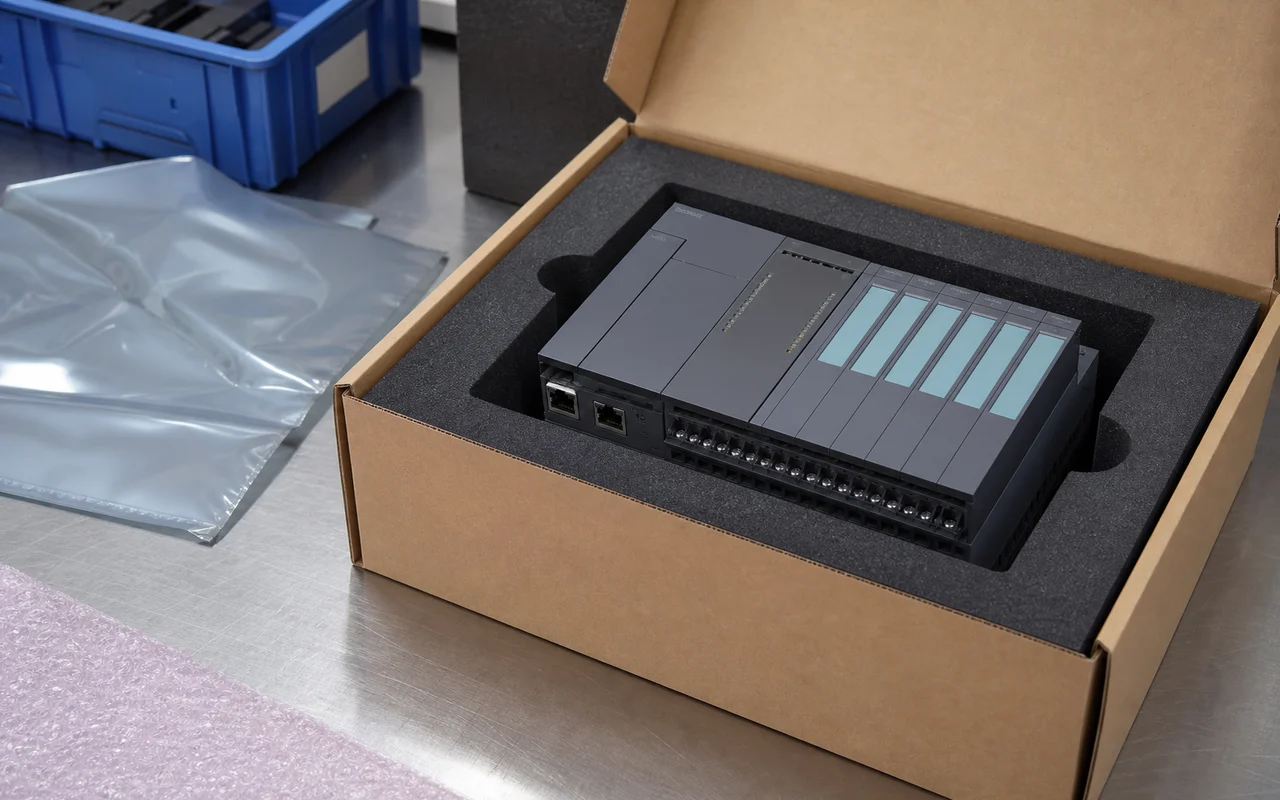 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.