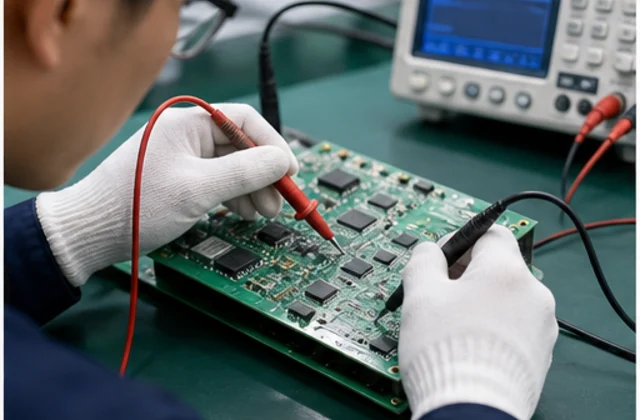
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
Slimpak G128 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.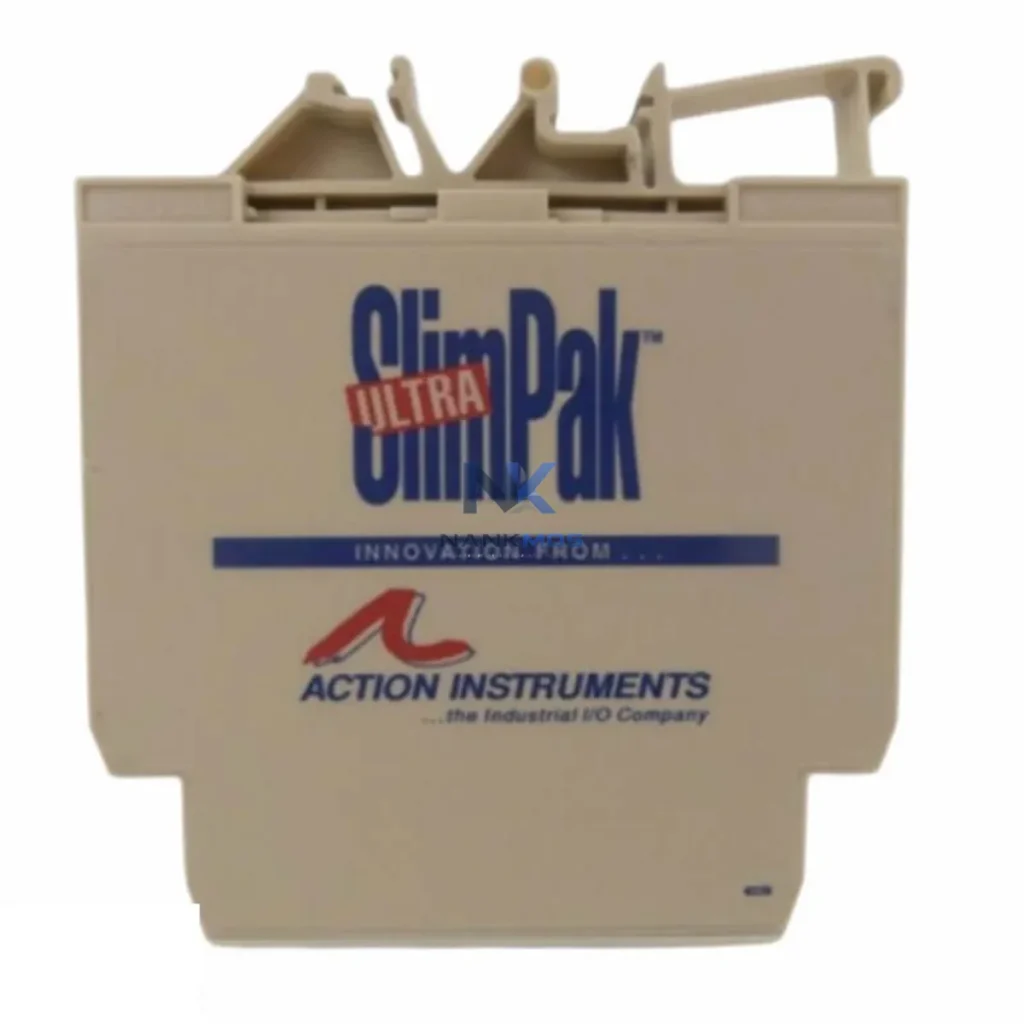
Slimpak G128 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | Slimpak |
|---|---|
| Application | Industrial Automation Maintenance |
| Part Number / Model | G128 |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Automation, Control & Flow Devices |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The Slimpak G128 is a precision-engineered network-linked signal conditioner designed for industrial environments where reliable data transmission, protocol compatibility, and real-time signal integrity are non-negotiable. As part of the proven Slimpak G-Series platform, the G128 bridges the gap between field-level instrumentation and upper-layer control systems — enabling seamless data flow from sensors and transmitters through to PLCs, SCADA platforms, HMI panels, and enterprise MES/ERP layers. Whether deployed in process manufacturing, discrete automation, or hybrid smart factory architectures, the G128 delivers the signal conditioning and network connectivity that modern industrial data chains demand.
In a modern smart factory, the Slimpak G128 operates at the critical junction between physical process signals and digital control infrastructure. The data flow begins at the field level: pressure transmitters, flow meters, temperature sensors, and level probes generate 4–20 mA or voltage signals that must be accurately conditioned, isolated, and transmitted upstream without noise, ground loops, or signal degradation.
The G128 accepts these raw field signals and delivers clean, galvanically isolated analog outputs directly to the analog input modules of PLCs such as the Siemens S7-300/S7-400 series or Allen-Bradley ControlLogix platforms. From the PLC, process values are passed via Modbus RTU or Modbus TCP — often through an industrial Ethernet switch or managed switch infrastructure — to SCADA servers running platforms such as Wonderware, Ignition, or Siemens WinCC. At this layer, the G128's conditioned signal becomes a live data point on operator dashboards, trend charts, and alarm management screens.
For installations requiring remote I/O expansion, the G128 pairs naturally with distributed I/O modules such as the Wago 750-series or Phoenix Contact Inline remote I/O nodes, which aggregate multiple conditioned signals and forward them over PROFIBUS DP or EtherNet/IP to the main PLC rack. In edge computing architectures, the G128's output feeds into edge gateways — such as the Moxa MGate series or Advantech ADAM-6000 series — which perform local data pre-processing, protocol conversion from analog to OPC-UA or MQTT, and push structured data packets to cloud-based MES or IIoT platforms.
HMI panels installed at machine stations — including Siemens TP700 Comfort or Weintek cMT series — receive real-time process values from the SCADA layer, enabling operators to monitor conditioned signals from the G128 without direct wiring to the field device. Variable frequency drives (VFDs) controlling pump and fan loads also benefit from the G128's isolated analog output, as clean 4–20 mA speed reference signals eliminate interference-induced drive faults common in electrically noisy environments.
For power distribution within the control panel, the G128 operates reliably alongside Phoenix Contact QUINT or Puls PIANO DIN rail power supplies, ensuring stable 24 V DC supply even under fluctuating load conditions. The complete data chain — from sensor signal through G128 conditioning, PLC acquisition, network transmission, SCADA visualization, and edge analytics — forms the backbone of a transparent, connected production environment.
Protocol fragmentation is one of the most persistent challenges in brownfield automation upgrades. Legacy field devices output raw 4–20 mA signals that cannot be directly consumed by modern Ethernet-based control systems. The Slimpak G128 resolves this by providing a clean, isolated analog bridge that any PLC analog input module can read — regardless of the upstream network protocol. This eliminates the need for costly field device replacement and allows existing instrumentation to participate fully in a Modbus TCP, PROFINET, or EtherNet/IP network architecture via the PLC layer.
Data islands form when field signals are conditioned locally but never integrated into the plant-wide data network. The G128's precise output accuracy (typically ±0.1% of span) ensures that SCADA historians receive high-fidelity process data, enabling meaningful trend analysis, KPI tracking, and predictive maintenance algorithms. Engineers can correlate G128-conditioned temperature or pressure readings with VFD load data and energy meter outputs to identify inefficiencies before they become failures.
Remote monitoring and diagnostics become practical when signal integrity is guaranteed at the source. With the G128 providing stable, noise-free analog outputs, remote SCADA operators can trust that alarm thresholds reflect true process conditions — not electrical interference artifacts. This is particularly valuable in multi-site operations where a central NOC monitors dozens of remote substations or process skids over WAN connections.
Production line transparency improves when every sensor signal is properly conditioned and network-accessible. The G128 enables plant managers to build complete digital twins of their process lines by ensuring that every 4–20 mA transmitter contributes accurate, real-time data to the SCADA/MES layer. Alarm tracking, shift reporting, and OEE calculations all depend on the signal quality that the G128 consistently delivers.
System scalability is built into the G128's DIN rail form factor and G-Series modular architecture. As production lines expand, additional G128 units can be added to the control panel without rewiring the field bus or reconfiguring the PLC network — making it a future-proof investment for growing automation infrastructure.
Q1: Does the Slimpak G128 support Modbus communication directly? The G128 provides isolated analog signal conditioning (4–20 mA / voltage output) rather than a direct Modbus serial port. However, its output connects to any PLC analog input module, and the PLC then exposes the conditioned value over Modbus RTU, Modbus TCP, PROFINET, or EtherNet/IP — making the G128 fully compatible with Modbus-based SCADA and HMI systems through the PLC layer.
Q2: How does the G128 ensure network stability and signal integrity in electrically noisy environments? The G128 features 3-way galvanic isolation between input, output, and power circuits. This eliminates ground loops, common-mode noise, and interference from variable frequency drives, contactors, and high-voltage switching equipment — ensuring that the analog signal reaching the PLC or remote I/O module is clean and stable regardless of panel noise conditions.
Q3: Can the G128 be integrated into existing SCADA and remote diagnostic systems without replacing field devices? Yes. The G128 is designed as a transparent signal conditioner that inserts into the existing 4–20 mA loop without requiring field device replacement. It conditions and re-transmits the signal to the control system, enabling full SCADA integration, remote monitoring, and alarm management while preserving the existing field wiring and instrumentation investment.
Q4: What warranty and pre-shipment testing does the G128 include? Every Slimpak G128 unit is covered by a 12-month warranty and undergoes functional testing prior to shipment. Units are held in verified in-stock inventory to support urgent project timelines. For procurement inquiries, technical specifications, or volume pricing, contact NANKMOS at [email protected] or +86 18359268345.
Functional Inspection100% tested on professional platforms to ensure stable performance.
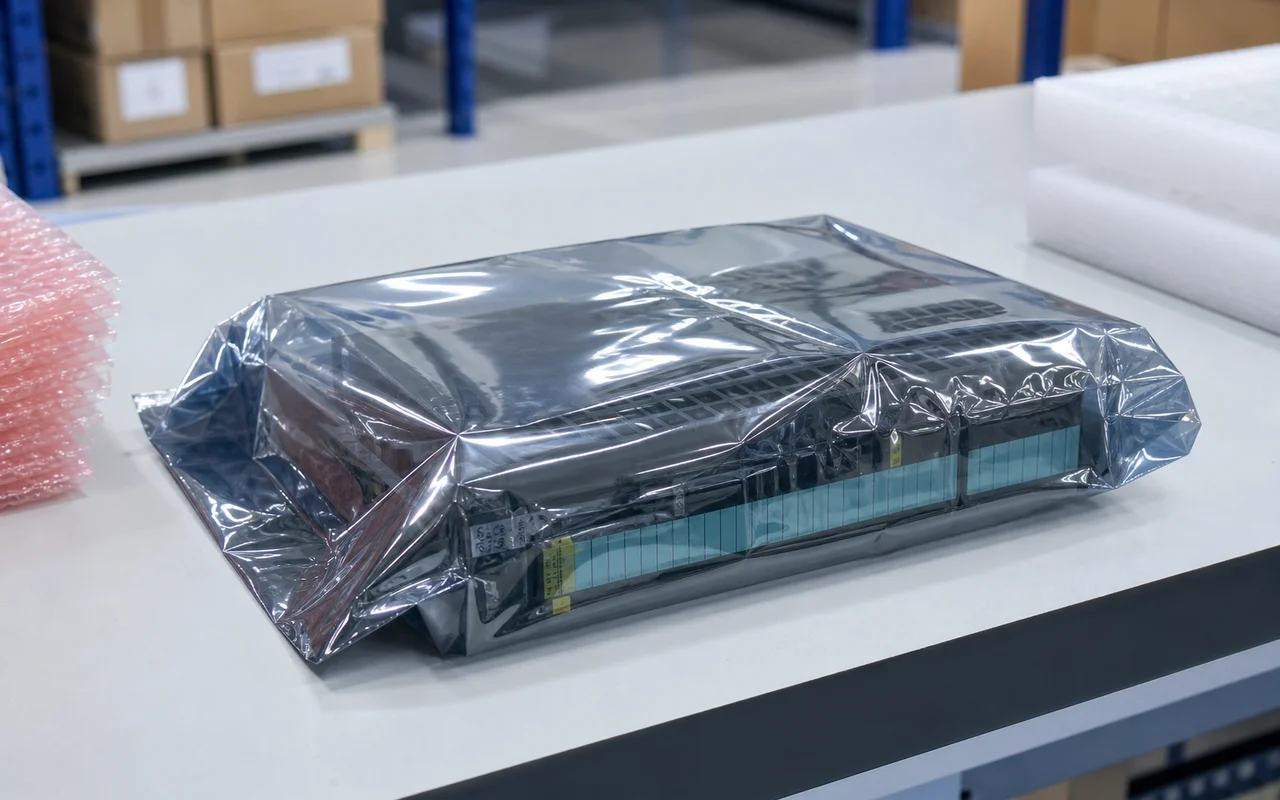 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
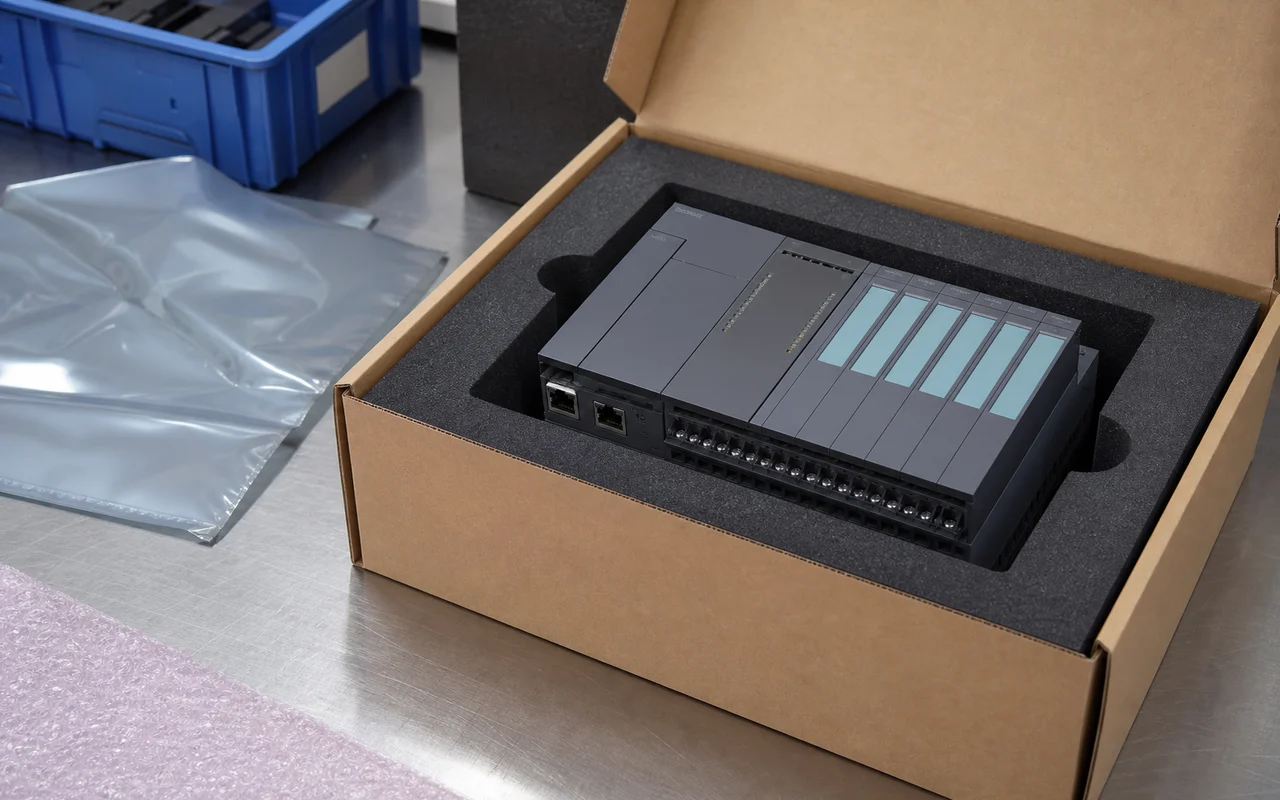 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.