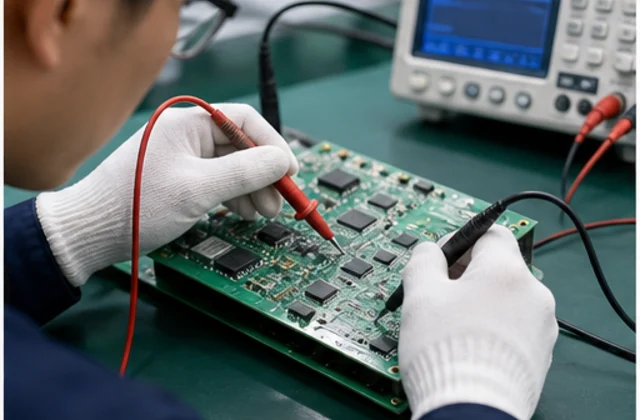
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
BKVIBRO VIBRO VC-1100 C11 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.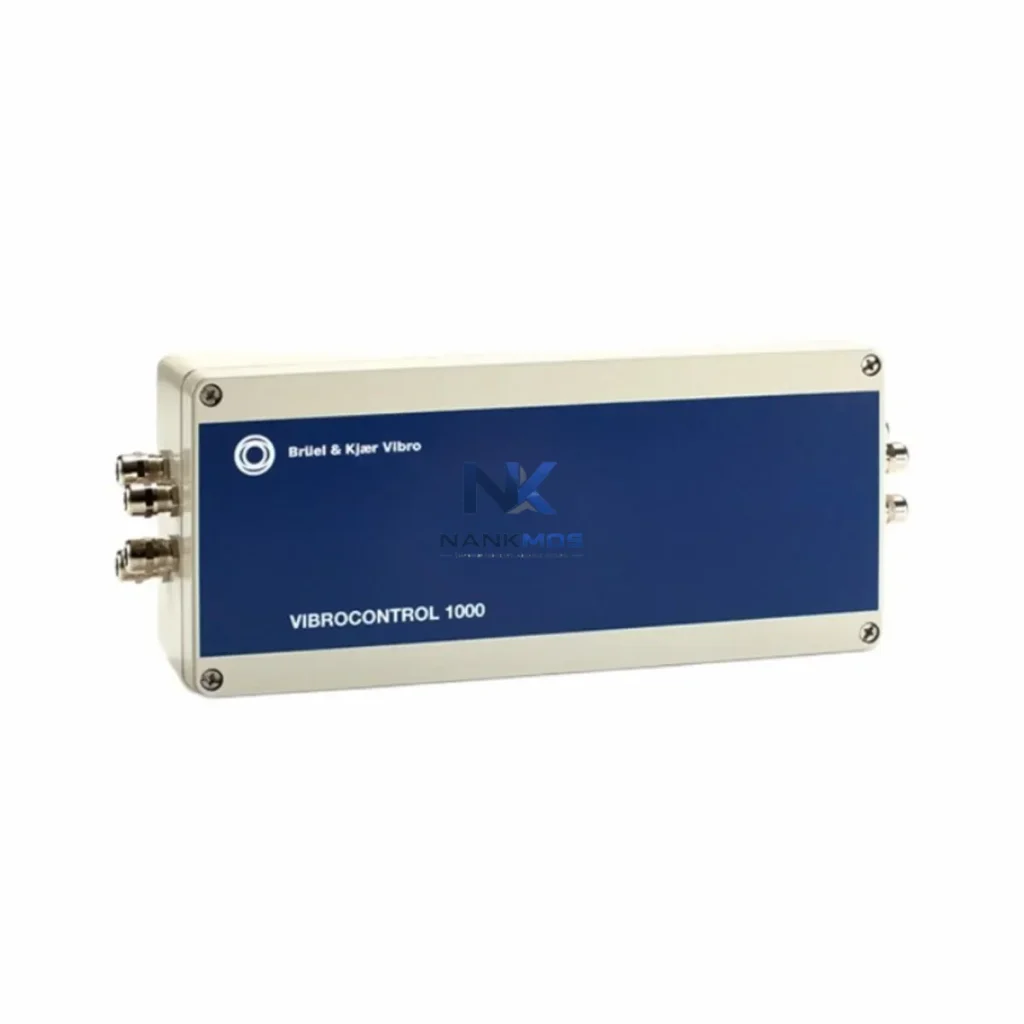
BKVIBRO VIBRO VC-1100 C11 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | BKVIBRO |
|---|---|
| Application | Turbine & Condition Monitoring |
| Part Number / Model | VIBRO VC-1100 C11 |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Monitoring Module |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The BKVIBRO VIBRO VC-1100 C11 is a precision vibration monitoring module engineered for energy-conscious industrial environments where motor health, load stability, and production line continuity are mission-critical. Designed to integrate seamlessly into modern automation architectures, the VC-1100 C11 delivers real-time vibration data that enables proactive energy management, reduces unnecessary motor runtime, and eliminates the hidden energy costs associated with mechanical degradation and unplanned downtime.
In smart manufacturing facilities, vibration anomalies in rotating equipment — motors, pumps, compressors, and conveyor drives — are among the leading causes of excess energy consumption. The BKVIBRO VC-1100 C11 addresses this directly by providing continuous, high-resolution vibration feedback that allows control systems to respond dynamically, adjusting drive output, modifying load profiles, and triggering maintenance workflows before energy waste escalates into equipment failure.
The BKVIBRO VC-1100 C11 is built to operate as an active participant in a power-aware automation strategy, not merely a passive sensor. When integrated with a Siemens S7-1500 PLC or equivalent programmable logic controller, the VC-1100 C11 feeds vibration amplitude and frequency data directly into the control loop, enabling the PLC to make real-time decisions about motor speed, load shedding, and drive modulation. This closed-loop approach eliminates the energy penalty of running motors at fixed speeds regardless of mechanical condition.
Paired with a variable frequency drive (VFD) such as the ABB ACS880 or Siemens SINAMICS G120, the VC-1100 C11 enables speed-adaptive motor control based on actual vibration signatures. When the module detects elevated vibration — a common indicator of bearing wear, imbalance, or misalignment — the VFD can automatically reduce motor speed to a safe operating range, cutting energy consumption by 20–40% compared to fixed-speed operation under fault conditions. This integration is particularly effective in pump and fan applications where affinity laws amplify the energy savings of even modest speed reductions.
For servo-driven axes on CNC machining centers or robotic assembly lines, the VC-1100 C11 complements servo drive systems by providing mechanical health data that the motion controller can use to adjust torque limits and acceleration profiles. Excessive vibration on a servo axis often indicates mechanical resonance or tooling wear; by detecting this early, the system avoids the energy-intensive recovery cycles that follow unexpected axis faults.
The VC-1100 C11 also integrates naturally with power monitoring modules such as the BKVIBRO PM series or third-party power quality analyzers connected via Modbus RTU or PROFIBUS DP. By correlating vibration data with real-time power consumption readings, energy managers gain a composite view of equipment health and energy efficiency — identifying machines that consume disproportionate power relative to their mechanical output. This correlation is the foundation of effective energy KPI tracking within an ISO 50001-aligned energy management system.
On the I/O layer, the VC-1100 C11 connects to distributed I/O modules within a PROFINET or EtherNet/IP network, making its vibration data available to the broader control architecture without dedicated wiring runs to the central PLC. HMI panels — including BKVIBRO touch panels or Siemens SIMATIC HMI units — can display live vibration trends alongside energy consumption dashboards, giving operators a unified view of machine health and energy performance at the line level.
For facilities running SCADA platforms such as Wonderware InTouch or Ignition by Inductive Automation, the VC-1100 C11 data stream integrates via OPC-UA or standard industrial communication gateways, enabling plant-wide energy monitoring and vibration trend analysis across multiple production cells simultaneously.
In high-throughput production environments, the BKVIBRO VC-1100 C11 delivers measurable energy optimization across three key dimensions: reactive energy reduction, thermal load management, and production rhythm stabilization.
Reactive energy reduction is achieved by eliminating the root causes of power factor degradation. Motors operating with mechanical faults — imbalance, bearing defects, or misalignment — draw higher reactive current as they struggle to maintain torque. The VC-1100 C11 detects these conditions before they reach the threshold of visible performance degradation, allowing maintenance teams to intervene during scheduled downtime rather than during production. The result is a consistently healthier power factor across the motor fleet, reducing reactive energy charges and lowering the burden on power factor correction capacitor banks.
Thermal load management is a direct beneficiary of vibration-based condition monitoring. Mechanical faults generate excess heat in motor windings, bearings, and gearboxes — heat that must be removed by cooling systems that themselves consume energy. By catching faults early, the VC-1100 C11 reduces the thermal load on both the monitored equipment and the facility's HVAC and cooling infrastructure. In densely packed control panels and motor control centers (MCCs), this thermal relief translates directly into reduced cooling energy and extended component lifespan.
Production rhythm stabilization is perhaps the most commercially significant energy benefit. Unplanned stoppages caused by vibration-induced failures disrupt production line takt time, forcing restart sequences that consume surge energy and generate thermal stress on drives and motors. The VC-1100 C11 enables a predictive maintenance posture that keeps production lines running at their designed takt rate, eliminating the energy and productivity losses associated with reactive maintenance cycles. Facilities that have implemented continuous vibration monitoring report reductions in unplanned downtime of 30–60%, with corresponding improvements in overall equipment effectiveness (OEE) and energy intensity per unit produced.
In-stock units are available for immediate dispatch, fully tested and verified against BKVIBRO factory specifications. Each VC-1100 C11 ships with a 12-month warranty covering manufacturing defects and performance deviations, supported by NANKMOS technical staff for integration guidance and replacement logistics.
Q1: How does the BKVIBRO VIBRO VC-1100 C11 contribute to measurable energy savings on a production line?The VC-1100 C11 enables energy savings by detecting mechanical faults — bearing wear, imbalance, misalignment — before they cause motors and drives to operate inefficiently. By feeding vibration data into the PLC and VFD control loop, the system can reduce motor speed, adjust load profiles, and schedule maintenance during planned downtime, avoiding the energy penalties of fault-state operation and unplanned restart cycles.
Q2: Which control systems and communication protocols is the VC-1100 C11 compatible with?The VC-1100 C11 is compatible with major industrial automation platforms including Siemens SIMATIC, ABB Automation Builder, and Rockwell Automation architectures. It supports standard industrial communication protocols including Modbus RTU, PROFIBUS DP, and PROFINET, and can be integrated with SCADA systems via OPC-UA gateways. Consult the BKVIBRO VC-1100 series datasheet for full protocol compatibility details.
Q3: Can the VC-1100 C11 replace an existing vibration sensor or monitoring module from another brand?In most cases, yes. The VC-1100 C11 is designed with standard industrial signal outputs and mounting configurations that facilitate drop-in replacement of legacy vibration monitoring modules. For specific cross-reference requirements, NANKMOS technical support can assist with compatibility verification and provide replacement guidance based on your existing system architecture.
Q4: What does the 12-month warranty cover, and how is the unit tested before shipment?Each BKVIBRO VIBRO VC-1100 C11 unit undergoes functional testing prior to shipment, verifying vibration sensing accuracy, signal output integrity, and communication interface performance. The 12-month warranty covers manufacturing defects and performance deviations from published specifications. NANKMOS maintains in-stock inventory of the VC-1100 C11 to support rapid replacement under warranty and to minimize production line downtime in the event of a warranty claim.
Functional Inspection100% tested on professional platforms to ensure stable performance.
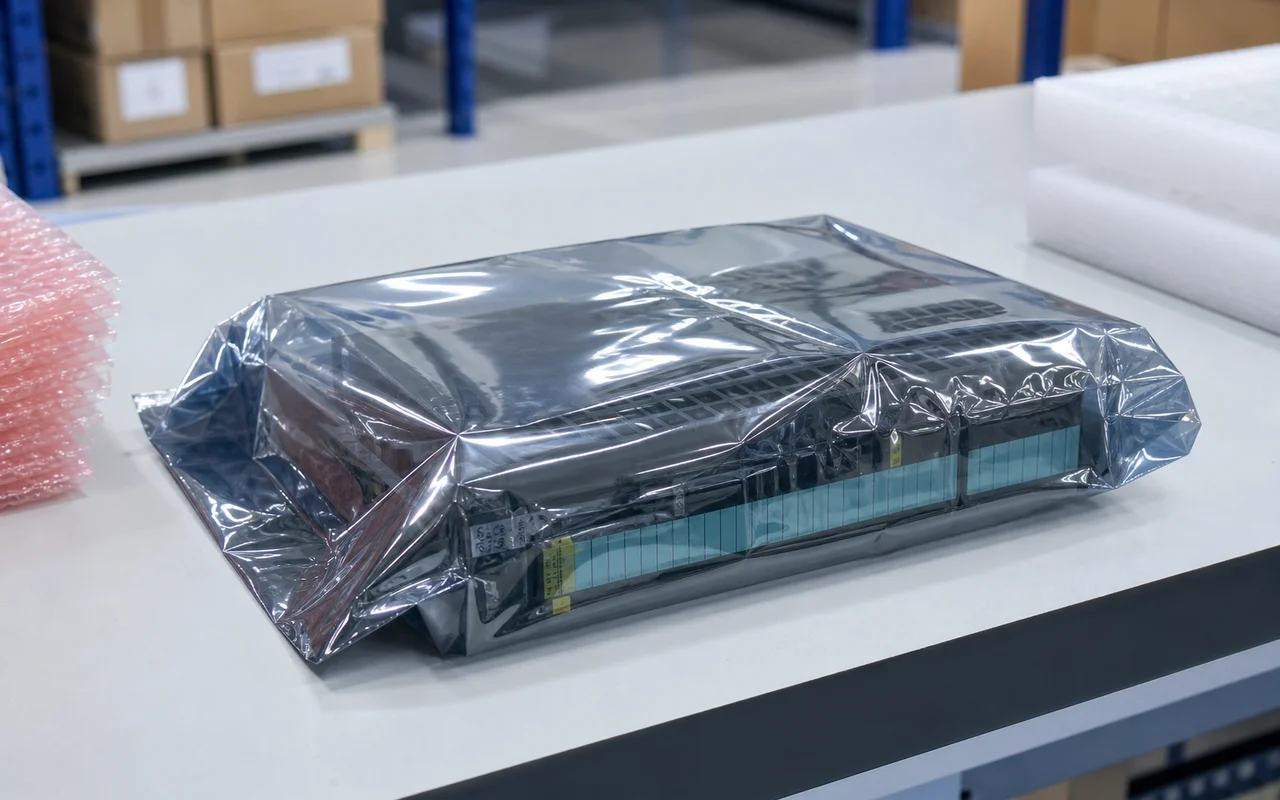 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
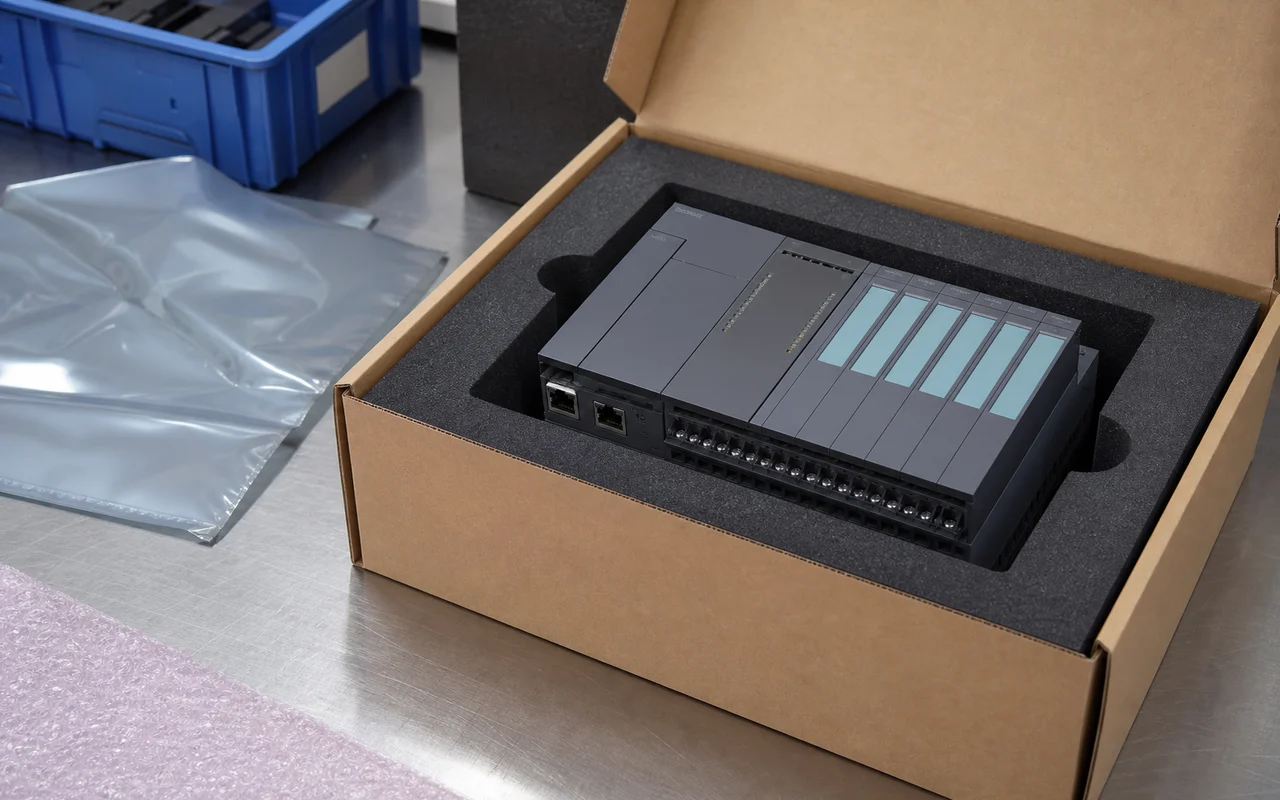 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
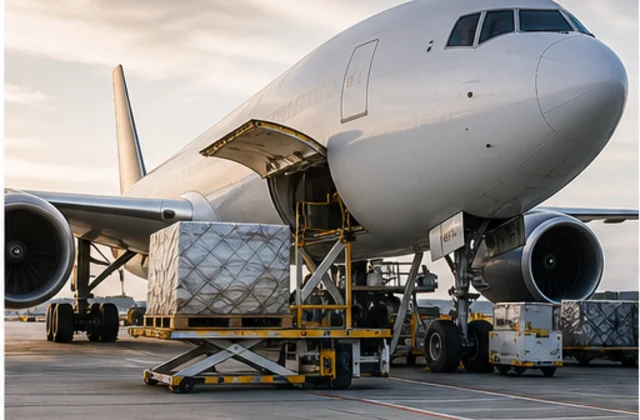 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.