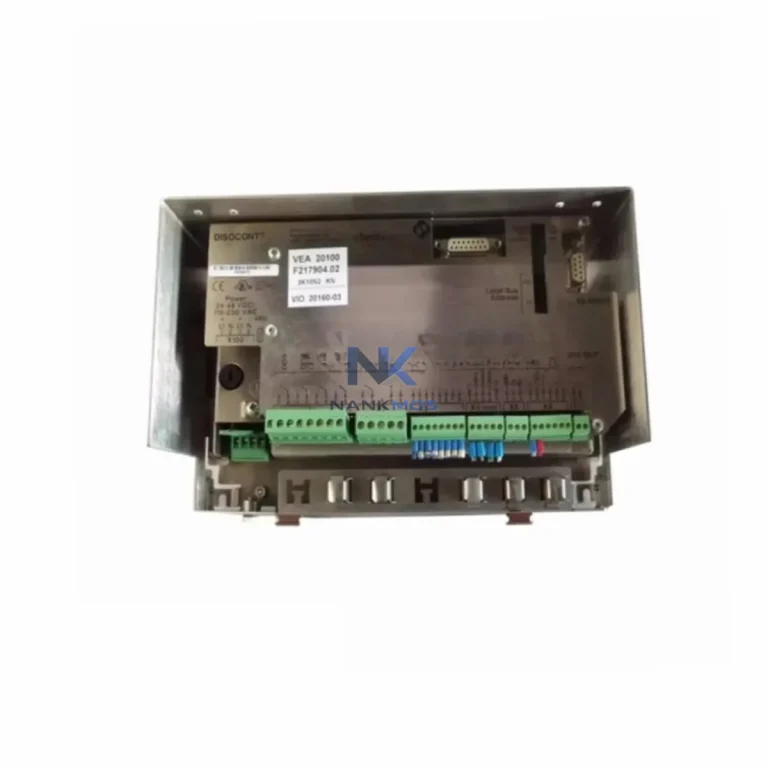
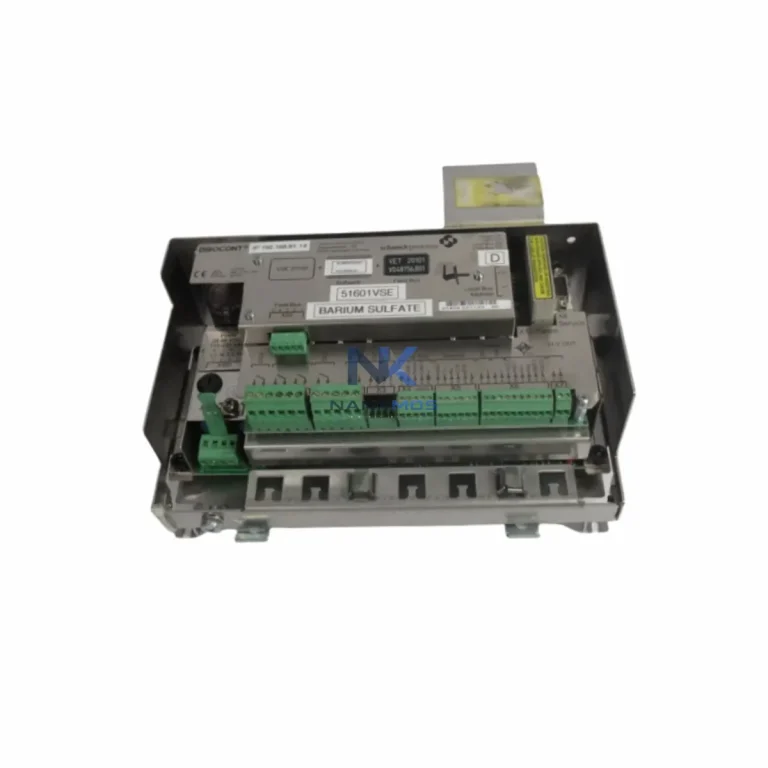
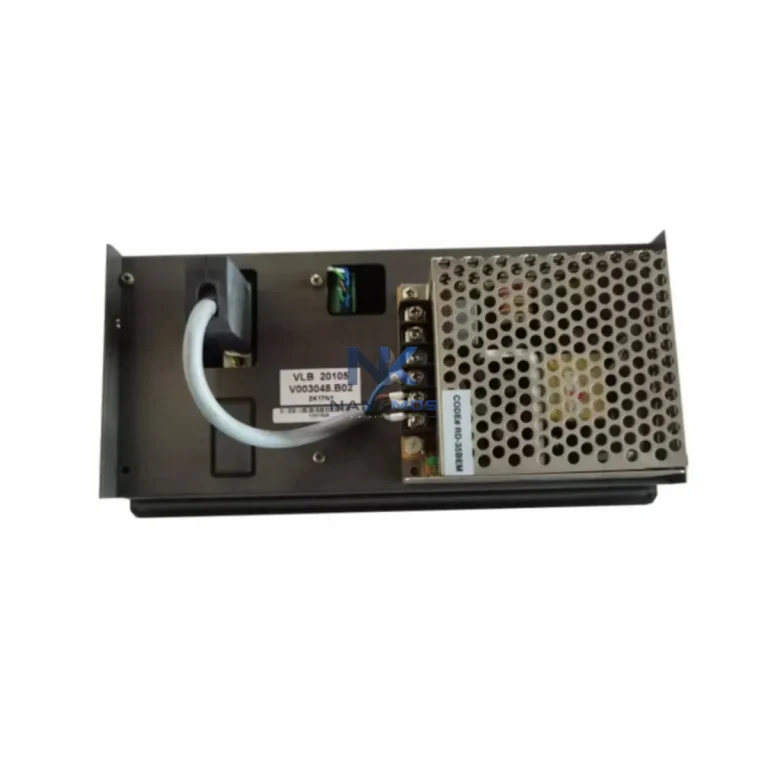
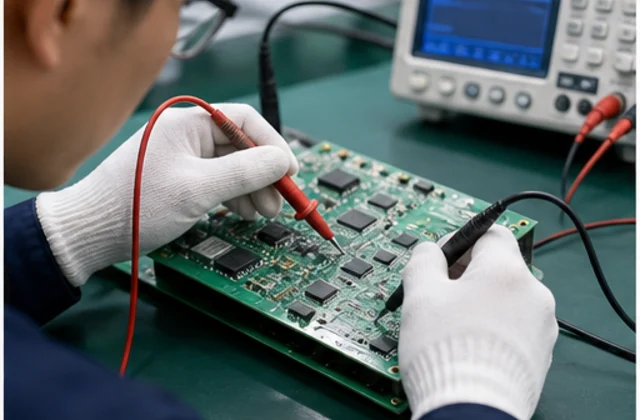
 Functional Inspection
100% tested on professional platforms to ensure stable performance.
Schenck VMD20150.xx V003853.B11 VMD20150 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
Brand names are used for identification only.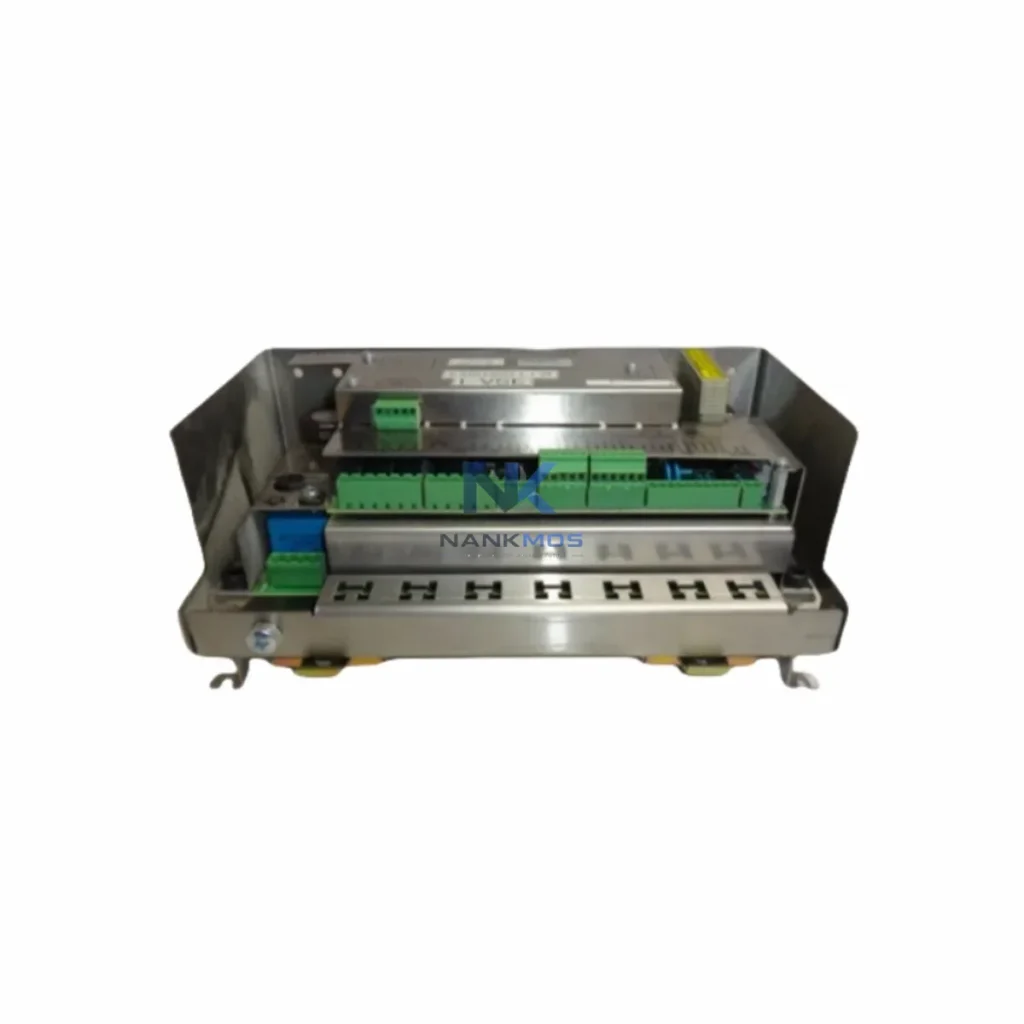
Schenck VMD20150.xx V003853.B11 VMD20150 is a NANKMOS industrial automation product record Listed under Other series series and Business & Industrial > Automation, Control & Flow Devices. Confirm condition, availability, lead time, compatibility and documentation by email inquiry.
| Manufacturer | Schenck |
|---|---|
| Application | Industrial Automation Maintenance |
| Part Number / Model | VMD20150.xx V003853.B11 VMD20150 |
| Compatible System | Confirmed by inquiry |
| Condition Options | To Confirm |
| Module Type | Automation, Control & Flow Devices |
| Warranty | 12 Months |
| Packaging | Anti-static Bag / Secure Box |
| Shipping Methods | DHL / FedEx / UPS / Air / Sea |
| Availability | To Confirm |
| Lead Time | To Confirm |
| Documentation | Part number and revision checked before quote |
The Schenck VMD20150 is a purpose-built industrial network interface and communication gateway designed to bridge Schenck Disocont weighing and feeding controllers with higher-level automation networks via Profibus DP. In modern smart factory environments where real-time data visibility, remote diagnostics, and seamless protocol interoperability are non-negotiable, the VMD20150 serves as the critical data link between field-level instrumentation and plant-wide control architectures.
Deployed across bulk material handling, continuous weighing, and gravimetric feeding applications, the VMD20150 enables Disocont controllers — including the Disocont Tersus and Disocont VS series — to communicate transparently with Siemens S7-300/S7-400 PLCs, Siemens S7-1500 TIA Portal systems, and third-party SCADA platforms such as WinCC, iFIX, and Ignition. By converting proprietary Disocont process data into standard Profibus DP telegrams, the VMD20150 eliminates data silos and ensures that weighing, feeding rate, setpoint, and alarm data flow continuously from the field to the control room.
From signal acquisition at the load cell or belt scale sensor level, the Disocont controller aggregates process values and passes them through the VMD20150 gateway into the Profibus DP network segment. Upstream, a Siemens ET 200SP or ET 200M remote I/O station may reside on the same Profibus segment, collecting additional analog and digital signals from proximity sensors, flow transmitters, and motor feedback devices. The PLC master — typically a Siemens S7-400H or S7-1500 — polls all Profibus slaves cyclically, ensuring deterministic data delivery with sub-10ms cycle times suitable for closed-loop control.
At the SCADA and HMI layer, operators gain full visibility into Disocont feeding rates, totalized weights, deviation alarms, and drive status through standard OPC DA/UA data servers connected to the Profibus master. Wonderware System Platform, Siemens WinCC OA, or Rockwell FactoryTalk View SE can all consume this data for real-time dashboards, trend logging, and alarm management. The VMD20150 thus transforms an otherwise isolated Disocont subsystem into a fully networked node within the plant's digital backbone.
Remote diagnostics capabilities are equally significant. Maintenance engineers can interrogate Disocont controller parameters, calibration data, and fault histories through the Profibus network without physical access to the field panel. When integrated with an industrial edge gateway — such as a Moxa MGate or Hilscher netTAP — the Profibus segment data can be further tunneled to cloud-based analytics platforms, enabling predictive maintenance models based on belt drift trends, motor load signatures, and feed rate deviations.
For facilities running mixed-protocol environments, the VMD20150 pairs naturally with Profibus-to-Ethernet gateways or Profibus-to-PROFINET couplers, allowing Disocont data to reach ERP and MES systems via standard TCP/IP infrastructure. This architecture supports Industry 4.0 data transparency requirements without requiring a full controller replacement or costly re-engineering of the existing Disocont installation.
Every VMD20150 unit supplied by NANKMOS undergoes pre-shipment functional testing, verifying Profibus DP communication integrity, slave address configuration, and data mapping accuracy before dispatch. Stock availability is maintained to support urgent project timelines, and all units are covered by a 12-month warranty from the date of shipment.
In a typical smart factory deployment, the VMD20150 occupies the protocol boundary between the Disocont process controller and the plant Profibus DP backbone. At the field level, load cells and belt speed sensors feed raw signals into the Disocont Tersus controller, which calculates real-time feed rates, totalized weights, and deviation values. The VMD20150 maps these process variables into Profibus DP input/output data areas, making them immediately accessible to the Siemens S7-1500 PLC acting as Profibus master.
On the same Profibus segment, a Siemens ET 200SP distributed I/O station collects digital status signals from motor contactors, valve feedback, and emergency stop circuits. A Siemens SINAMICS G120 variable frequency drive — also Profibus-capable — reports motor speed, torque, and fault codes to the same PLC master, enabling coordinated control of the feeding drive and the Disocont setpoint in a single scan cycle. This tight integration eliminates the latency and data loss associated with serial point-to-point wiring between the drive and the controller.
Further upstream, a Siemens S7-400H redundant PLC aggregates data from multiple Profibus segments across the plant, passing consolidated process data to a WinCC SCADA server via Industrial Ethernet (PROFINET). Operators at HMI panels — running Siemens TP1500 Comfort or similar — monitor live feed rates, alarm states, and calibration status in real time. Historian servers log all process variables at configurable scan rates, supporting quality traceability and regulatory compliance reporting.
For remote diagnostics, a Moxa MGate MB3480 Modbus-to-Profibus gateway or a Hilscher netTAP NT 100-RE-DP bridges the Profibus segment to an Ethernet backbone, allowing remote engineers to access Disocont parameters and VMD20150 diagnostic registers via a VPN-secured connection. This architecture supports predictive maintenance workflows without requiring on-site intervention, reducing mean time to repair and minimizing unplanned downtime in continuous production environments.
Many bulk material handling and process weighing installations suffer from persistent data gaps: Disocont controllers operate as isolated islands, unable to share process data with plant-wide SCADA systems, ERP platforms, or remote monitoring tools. The VMD20150 directly resolves this by providing a standards-compliant Profibus DP interface that integrates Disocont data into the existing automation network without modifying the controller's core configuration.
Protocol fragmentation — where Disocont proprietary communication coexists with Profibus, PROFINET, and Modbus segments — is addressed through the VMD20150's transparent data mapping. Engineers define the Profibus GSD file configuration once, and the gateway handles all cyclic data exchange autonomously, freeing PLC programmers from custom serial communication blocks and reducing software maintenance overhead.
Data island elimination extends to alarm management: Disocont fault codes, calibration deviation alerts, and feeder overload warnings are now visible in the plant SCADA alarm server alongside PLC and drive faults, enabling unified alarm rationalization and faster root-cause analysis. Production line transparency improves as feeding rate trends, batch totals, and setpoint adherence data become available for MES integration and OEE calculation.
System expansion is straightforward: additional Disocont controllers can be networked on the same Profibus segment using additional VMD20150 gateways, each assigned a unique Profibus slave address. The PLC master's configuration is updated via the GSD file, and the new data points are immediately available in the SCADA historian — no new cabling infrastructure required beyond the Profibus trunk extension.
Q1: What Profibus DP transmission speeds does the VMD20150 support, and will it cause latency in closed-loop control?The VMD20150 supports all standard Profibus DP baud rates from 9.6 kbps to 12 Mbps with automatic baud rate detection. At 1.5 Mbps — a common plant standard — cyclic data exchange completes within one Profibus bus cycle, typically under 5ms for segments with fewer than 32 slaves. This is well within the tolerance of most gravimetric feeding control loops, which operate on 100ms–500ms setpoint update intervals.
Q2: Is the VMD20150 compatible with both Siemens S7-300/400 and S7-1500 TIA Portal Profibus masters?Yes. The VMD20150 is supplied with a standard GSD file that is importable into both STEP 7 Classic (S7-300/400) and TIA Portal V13 and later (S7-1500). The slave configuration, I/O data length, and diagnostic functions are fully supported in both engineering environments. No firmware modification is required for TIA Portal compatibility.
Q3: Can the VMD20150 support remote diagnostics and parameter access without physical access to the Disocont panel?Yes. Through the Profibus DP V1 acyclic services supported by the VMD20150, a Profibus master with DP V1 capability can read and write Disocont parameters remotely. When combined with an Ethernet-to-Profibus gateway on the network, remote engineers can access diagnostic registers, calibration data, and fault logs via a secure VPN connection, eliminating the need for on-site visits for routine parameter checks.
Q4: What warranty and pre-shipment testing does NANKMOS provide for the VMD20150?All VMD20150 units supplied by NANKMOS carry a 12-month warranty from the shipment date. Prior to dispatch, each unit undergoes pre-shipment functional testing covering Profibus DP communication establishment, slave address verification, and data mapping validation against the supplied GSD configuration. Stock is maintained for prompt delivery to support urgent project and maintenance requirements.
Functional Inspection100% tested on professional platforms to ensure stable performance.
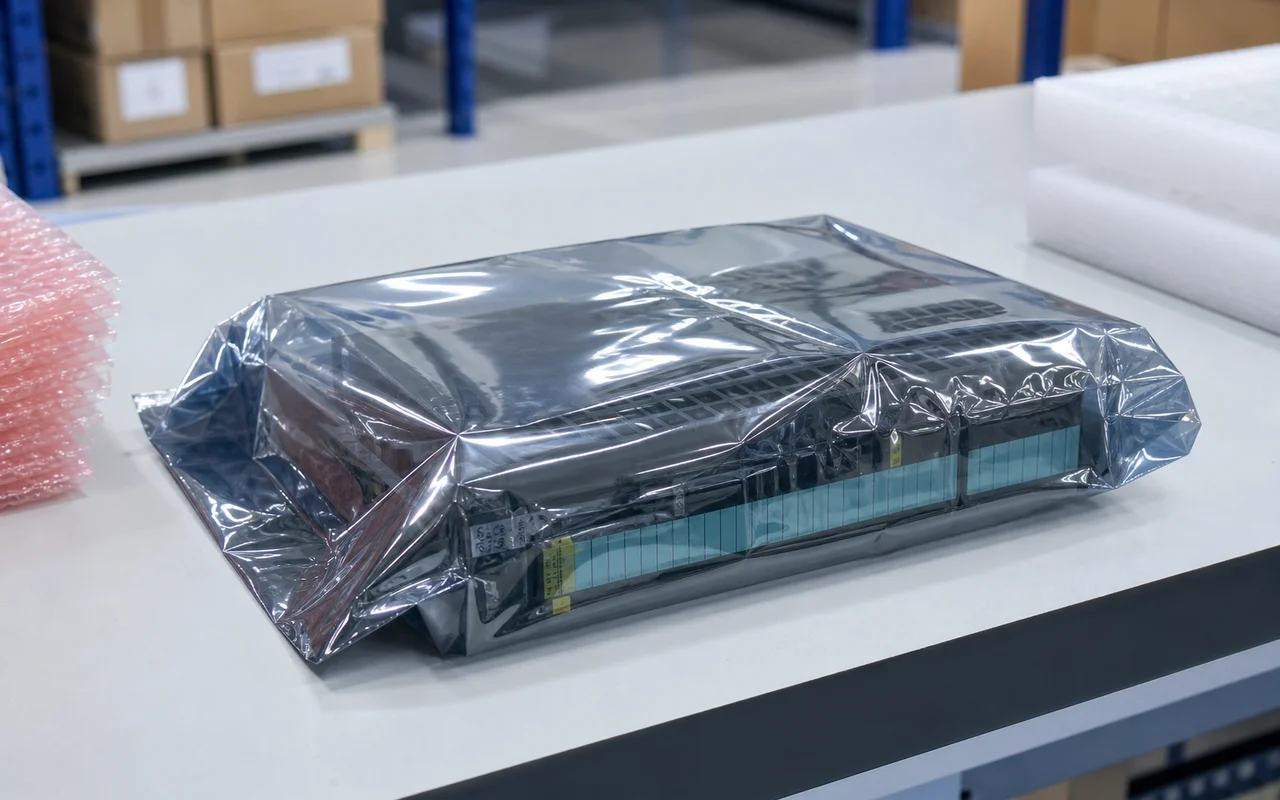 Anti-static Packaging
Modules are packed in anti-static bags to prevent electrostatic damage.
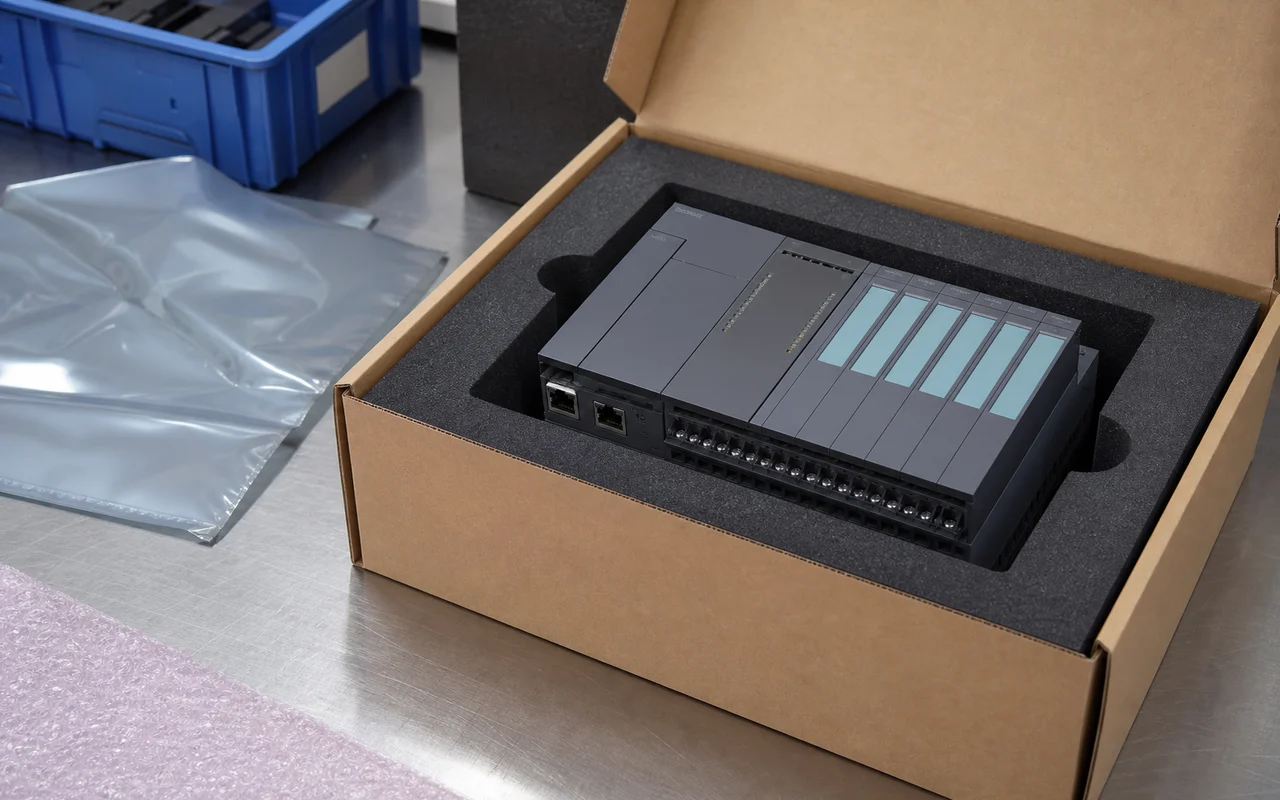 Secure Export Packing
Cushion protection and strong cartons ensure safe transportation.
 Worldwide Shipping
Global logistics network supports air, sea and express delivery.
 Documentation Check
Part number, revision and compatibility verified before shipment.
 After-sales Support
Professional technical support to help resolve your issues.